Mold Cost Guide · 2026
Injection Mold Cost: What You Actually Pay in China
An injection mold from China costs anywhere from about $1,500 to $80,000. The spread is not about labor rates. It is engineering scope. A single-cavity tool for a small part sits at the bottom. A large multi-cavity hardened tool with a hot runner and lifters sits at the top. Cavity count, steel grade, finish, tolerance and side actions move the number far more than wages ever will. This guide shows the cost of an injection mold by tool type, where the money goes and how to read a quote.
Quick answer: most plastic injection molds we build cost $1,500–80,000. Simple single-cavity tools start around $1,500. Medium multi-cavity production tools usually run $15,000–30,000. Large hot runner tools reach $50,000–80,000. Build time is typically 35–55 days from DFM approval.
How Much Does an Injection Mold Cost?
The honest answer is a range, then a quote. Here is where most tools land at our shop in Huangyan. Use it to sanity-check a budget, not to replace a quote on your own part.
Injection mold cost examples by tool type
| Tool type | Typical example | Typical cost (USD) |
|---|---|---|
| Simple single-cavity, no side actions | Small cap, clip or cover | $1,500–5,000 |
| Moderate tool, 1–2 cavities, a few side actions | Electronics housing, handle | $5,000–15,000 |
| Medium multi-cavity production tool | Automotive interior part | $15,000–30,000 |
| Large or hot runner production tool | Bumper, appliance panel | $30,000–80,000 |
Planning ranges, not a quote. Your geometry, steel and cavity count set the real number.
Why does the same part get quotes $3,000 apart? Usually the tools are not the same. One quote uses P20, the other H13. One has two cavities, the other four. One has a hot runner. Compare the spec sheets, not the bottom lines. More on that in why mold prices differ.
Injection Mold Cost Estimator
Pick part size, cavity count, complexity, steel, runner and finish. The estimator returns a one-time tooling range and compares China with North American and European pricing.
Not sure what to type in? Most buyers guess at wall thickness and volume. Work the other way round: tell us what the part does, and we work out size, material and tooling. It takes about five minutes and ends with a spec sheet you can send to any supplier. Work out my specification →
Injection Mold Cost Breakdown: Where the Money Goes
A mold is mostly steel, machine hours and skilled bench work. This is how a typical quote splits:
| Cost item | Typical share of mold price |
|---|---|
| Steel and mold base | 20–35% |
| Machining (CNC, EDM, engraving) | 25–40% |
| Fitting and assembly (bench work) | 15–20% |
| Mold design | 5–10% |
| Tax and profit | 20–30% |
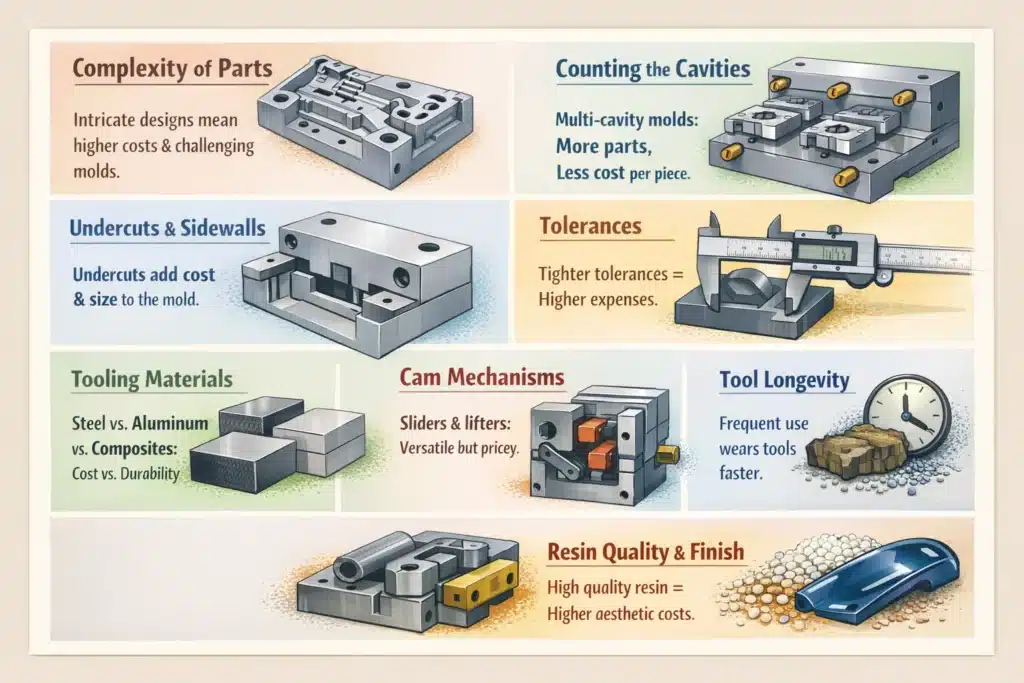
Machining is the biggest lever. Every slider, lifter and deep rib adds CNC and EDM hours. That is why design changes before steel is cut save more than any discount you can negotiate later.
What Drives Plastic Injection Mold Cost
Most of the gap between two quotes comes down to about seven engineering calls. Read each quote against these, not against each other.
Part size and envelope. Bigger part, bigger base, more steel to cut. Size also sets the press tonnage. That can shift the economics of the whole program before a single chip is made.
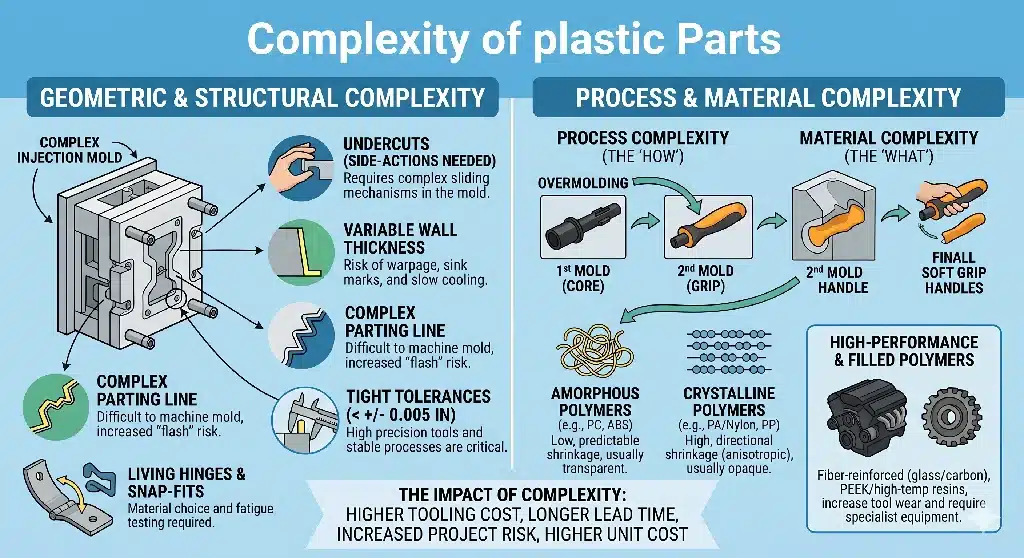
Geometry and undercuts. Every undercut buys you a lifter or a slider. Each one often adds $500 or more, makes the mold bigger and adds wear points. Internal threads buy you an unscrewing unit. I have seen a 2 mm change to a snap feature delete a whole side action. This is why DFM feedback pays for itself before steel is cut.
Cavitation. Cavity count follows annual volume and target cycle time. It is not a preference. More cavities mean a larger base and tighter balancing, so the tool costs more up front. That cost spreads over far more parts, so the piece price drops. Pick wrong in either direction and you overpay.
Resin and tool steel. The part material picks the steel for you. Glass-filled grades chew through soft steel and need hardened tooling. PVC, POM and flame-retardant compounds pit unsuitable steel and call for stainless or surface treatment. Steel grade governs guaranteed shot count, so it is matched to volume, not guessed.
Surface finish. High-gloss optical surfaces need premium steel and hand polishing. Textures need etching. Both add labor. Finish is one of the easiest lines to over-spec. Ask what the part needs to do, not what looks impressive on a drawing.
Tolerances. Tight, frequently checked dimensions push up machining time and inspection labor. They also force balanced cooling so warpage stays in spec. Count the critical-to-function dimensions on your print. That number is a direct cost driver. See our note on molding tolerances.
Cooling, gating and components. Good cooling and gate placement shorten the cycle and stabilize quality. A 4-second cut over a million-shot program is real money. Hot runner and ejector brands move both the price and how easy the tool is to fix three years in. Wall thickness and gate choice matter too; see how wall thickness and gates affect mold cost.
| Cost driver | What it affects in the mold | Effect on tooling cost | Effect on piece-part cost |
|---|---|---|---|
| Part size / envelope | Mold base size, steel volume, clamp tonnage | Higher with size | Roughly neutral |
| Geometry / undercuts | Lifters, sliders, unscrewing units | Higher | Higher (cycle, maintenance) |
| Cavity count | Base size, balancing, precision | Higher | Lower (cost spread over more parts) |
| Tool steel grade | Hardness, corrosion resistance, lifespan | Higher | Lower over life (fewer repairs) |
| Resin (abrasive / corrosive) | Required steel and surface treatment | Higher | Varies |
| Surface finish | Steel choice, polishing or etching labor | Higher | Roughly neutral |
| Tolerance band | Machining precision, inspection, cooling | Higher | Roughly neutral |
| Tool type (2-plate / 3-plate / hot runner) | Runner and gating system | Hot runner higher | Hot runner lower (no runner scrap) |
| Cooling design | Channels, baffles, conformal cooling | Higher | Lower (shorter cycle) |
Aluminum vs Steel Injection Mold Cost
An aluminum injection mold costs less and cuts faster than steel. It also conducts heat well, so cycles can be short. The trade-off is wear. Aluminum suits prototypes, bridge runs and unfilled resins. It struggles with glass-filled grades and repeated lifter action.
Steel costs more up front and lasts far longer. Pre-hardened P20 and 718H are the workhorses for most production. Hardened H13 and stainless S136 handle high volume, abrasive or corrosive resins and mirror finishes.
- Under about 1,000 parts: aluminum is almost always the cheaper total.
- 1,000–10,000 parts: aluminum or P20, depending on resin and side actions.
- Above 10,000 parts: P20, 718H or H13 starts to pay for itself.
For short runs, see our low volume injection molding options. Steel grades are compared on our injection mould tooling page and in P20 vs 718H vs H13 vs S136.
Two-Plate vs Three-Plate vs Hot Runner: Where the Money Goes
This is the clearest case where the cheapest tooling quote is not the cheapest program.
A two-plate cold-runner tool is the cheapest to build. It also drops a runner on every shot. That runner is scrap unless you regrind it, and an operator usually separates it. Labor goes up. Cycle goes up.
A three-plate or hot runner tool costs more up front. It de-gates automatically, removes most runner scrap and runs fully automated. Over a high-volume run, the higher tool price comes back through lower piece cost and less wasted resin.
The break-even depends on annual volume, part value and resin price per kilo. That is why cavitation and tool type are decided with the molder, not specified by procurement alone. If your supplier will not run that math with you, that is your answer.
Two-Plate vs Three-Plate Mold
Same two-cavity part, both molds closed. Hover or tap any part or number.
Injection Mold Cost in China vs the US
Chinese tooling usually quotes well below comparable US or European tooling. Machining hours and bench work cost far less here, and steel and standard parts sit a short drive from the shop. The real gap swings with complexity, steel spec and how the tool is actually built. Run the estimator above with each region selected to see the spread for your tool. We break it down further in 7 truths about China vs US tooling costs.
Why the cheapest quote is rarely the cheapest mold
The trap is treating the headline saving as the full picture. A quote gets cut in predictable ways:
- Under-spec the steel, and a “production” tool is really prototype grade. It cracks early.
- Undersize the cooling, and you live with long cycles and warpage for the life of the program.
- Skip mold-flow simulation, and defects show up after the steel is cut.
- Use off-brand components, and spares take six weeks to source.
None of this shows in the headline price. All of it shows later. Two quotes for “the same mold” can describe two different tools. The only honest comparison uses a matched spec sheet: steel grade, guaranteed shot count, cavitation, finish and named component brands. See our red flags guide and how to compare injection molding quotes from China.
How to Lower Your Injection Mold Cost
The biggest savings happen before steel is cut, not in the negotiation afterwards.
- Run DFM and mold-flow early. Uniform walls, generous draft and removable undercuts can each delete a side action.
- Match cavitation to real volume. Do not pay for capacity you will never use. Do not cap a program that needs to scale.
- Spec steel against expected shot count. Over-spec a low-volume part and you waste money. Under-spec a high-volume part and the tool dies before it pays back.
- Tighten only what matters. Hold tight tolerances and premium finishes only where the part needs them.
- Simplify geometry. Flat run-outs and simple features are easier to cut, inspect and maintain.
- Standardize components. Named hot runner and ejector brands keep spares available, so the tool stays serviceable anywhere.
- Use a family mold for small related parts. One tool, one setup, several parts per shot.
Ways to cut the cost per part, such as cycle time, automation and scrap, are covered in our injection molding cost per part guide.
What to Send for an Accurate Mold Quote
Do not leave tool buying to procurement alone. Several of these choices carry engineering consequences a purchasing team cannot weigh. Define the spec before the RFQ, so every supplier prices the same tool.
- 2D drawings and 3D CAD files (STEP or IGES)
- Resin, plus any fillers or flame-retardant additives
- Annual and lifetime volume, and required mold life in shots
- Critical tolerances and their values
- Surface finish: gloss, texture and cosmetic faces
- Preferred cavitation and tool type (2-plate, 3-plate, hot runner)
- Steel grade and component brand expectations
- Gate restrictions and target cycle time
- A sample part, if you have one
With this defined, two quotes can finally be compared on equal terms. Start from our injection molding RFQ template.
Mold Cost vs Part Cost
Mold cost is a one-time investment. Part cost is what you pay per piece, every order: resin, press time, labor, scrap and freight. A cheaper mold can raise part cost for years. A pricier multi-cavity tool can lower it.
So judge a mold quote by total cost at your real annual volume. For the per-piece side, read our guide to injection molding cost per part. On a tight budget? See how small businesses can afford tooling.
Frequently Asked Questions
How much does an injection mold cost in China?
Most molds we build cost $1,500–80,000. A simple single-cavity tool for a small part starts around $1,500. A medium multi-cavity production tool usually runs $15,000–30,000. Large hot runner tools can reach $50,000–80,000. You need a drawing or 3D file for a firm quote.
How much does a plastic mold cost for a small part?
A small part with no undercuts, in a single-cavity tool, usually costs $1,500–5,000. Side actions, extra cavities, hardened steel or a high-gloss finish push it higher.
Why are Chinese mold prices lower than Western suppliers?
Mostly lower machining and bench labor costs, plus a dense local supply of steel and standard parts. Labor cost alone should not decide the buy. Steel grade, build quality and tool life matter far more to total cost.
Is a cheaper mold quote always a better deal?
No. A lower quote often means lighter steel, undersized cooling, skipped mold-flow or off-brand components. Those savings come back as downtime, scrap and repairs. Compare matched specifications, not headline prices.
What is the cost difference between two-plate, three-plate and hot runner tooling?
A two-plate cold-runner tool is the cheapest to build, but it makes runner scrap and usually needs an operator. Three-plate and hot runner tools cost more up front. They de-gate automatically, cut runner waste and support automation. On high-volume runs, the higher tool price usually pays back through lower piece cost.
How many cavities should my mold have?
Size cavitation to annual volume and target cycle time. More cavities raise tooling cost but lower piece price. Too many or too few is a common reason buyers overpay. Decide it with the molder.
Is an aluminum injection mold cheaper than steel?
Yes, up front. Aluminum cuts faster and costs less, which suits prototypes and short runs. It wears faster, especially with glass-filled resins. Above roughly 10,000 parts, a steel tool usually gives the lower total cost.
How long does it take to build an injection mold?
Typically 35–55 days from DFM approval. Simple tools can be faster. Large multi-cavity hot runner tools take longer.
Do I own the mold after I pay for it?
Yes. If you pay for the tooling, you own 100% of it, and you can move it to another molder if you ever need to.
Get a Line-Itemed Mold Quote
Send your part drawing or 3D file. We send back a quote with steel grade, cavitation, tool type and guaranteed shot count spelled out. Compare it against anyone.
Request a Mold Quote →