Vacuum casting diagram by Topworks Plastic Mold
Short Runs · Rapid Tooling · Huangyan, China
Low Volume Injection Molding in China
Low volume injection molding means real plastic parts in short runs, usually 100 to 10,000 pieces. They are molded on a soft or semi-hard tool instead of full production steel. You skip most of the tooling bill. You get parts in the actual resin your customer will hold, weeks sooner than a production program allows. This page explains how it works, what drives the cost, where the limits sit, and why so many buyers run these jobs in China.

100–10,000 parts: The range most of our low volume jobs fall in.
Aluminum or P20: Typical tool steel for short runs, often as inserts in a master mold shoe.
About 3 weeks: Typical time to a first T1 sample on a straightforward part.
100–500 pieces: Typical minimum order, depending on part size, resin and tool route.
14 presses, 80–1,000 tons: From a 30 g handheld housing up to a 2 kg automotive bracket.
Low Volume Molding, CNC or 3D Printing?
Quantity decides most of it. Move the slider to your batch size and see where each process lands on feasibility and unit cost.
| Quantity | Usual best route |
|---|---|
| 1–20 pcs | 3D printing for concept and fit checks |
| 20–100 pcs | 3D printing, CNC or vacuum casting |
| 100–1,000 pcs | CNC or a low volume injection mold |
| 1,000–10,000 pcs | Low volume injection molding |
| 10,000+ pcs | Production injection molding |
Below about 100 pieces, a mold rarely pays. Vacuum casting gives near-molded parts from a silicone tool in that range.
See our 3D printing and vacuum casting service, or compare all three in 3D printing vs CNC vs vacuum casting.
Our Low Volume Injection Molding Service
We run low volume injection molding for buyers in automotive, medical, consumer electronics and industrial equipment. Most short-run jobs land between 100 and 10,000 parts. From first quote to last shipment, the same engineer stays on your file.
Send your 3D CAD when ready, and we return a free quote with DFM feedback. STEP and X_T work best, and Parasolid works too.
Our engineers review every design before we cut steel. They check draft angles, wall thickness, gate location and shut-off faces. We flag what would cause sink, flash or warpage while it is still cheap to fix.
Material choice gets the same attention. Tell us what the part must do. We come back with two or three resin options and the trade-offs between them. UV exposure, flame rating, chemical contact and drop height drive the recommendation. Our material selection guide covers the basics.
For the mold itself, we match steel and structure to your shot count and tolerance band. Most low volume jobs run on P20 or aluminum inserts in a master shoe.
Need a physical part before we cut the mold? Choose 3D printing or CNC machining for the first article on our rapid prototype line. That step catches design problems while fixes still cost little.
We run flexible schedules and add second or third shifts when timing is tight. The shop has 14 injection machines from 80 to 1,000 tons of clamp force. That covers a 30 g handheld housing up to a 2 kg automotive bracket. Multi-material parts can also run short, through our overmolding work, including insert and 2K molding.
What Is Low Volume Injection Molding?
Low volume injection molding is short-run plastic production on a softer, cheaper mold, usually aluminum or P20, in batches under 10,000. You give up tool life. You gain speed and a much smaller tooling bill.

That trade fits prototypes, pilot runs, bridge production and short-life products. The cutoff is fuzzy. Most shops, ours included, treat anything under 1,000 parts as clearly low volume. From 1,000 to about 10,000, the call depends on cycle time, resin cost and how long the design has to live.
Buyers like it for one reason. The path from CAD to shippable parts gets shorter, and options stay open. If the first 500 sell, the mold keeps running. If they do not, you have not sunk tens of thousands into hardened steel.
Short Run Injection Molding: Where It Pays Off
The math works in specific situations. Here is where we see short run injection molding pay off.
Bridge between prototyping and mass production
A 3D-printed part proves geometry. It does not prove how resin behaves under real injection pressure and shrinkage. A low volume mold fills that gap. You get parts in the real grade of ABS, PC or PP. You test fit, finish, weight and assembly on the plastic your customer will hold. Most product teams catch at least one assembly issue here that the print never showed.
Low minimums cut your cash exposure
You do not need 100,000 parts to launch. You need enough to test the market. A single-cavity aluminum or P20 mold costs a fraction of a multi-cavity hardened tool. Per-piece cost runs higher, but upfront cash runs far lower, and parts arrive in weeks. For most early-stage products, that trade beats a lower piece price.
Get into new markets fast
Entering a new region means you do not yet know which SKU will sell. Short-run molding puts real product in your hands for a tradeshow, a pilot customer or a regional test. The tooling wait drops from months to weeks.
Short product lifecycles
Some parts will not be on the market in two years. Consumer electronics housings, seasonal items and limited-run gadgets all turn over fast. Building a million-shot hardened mold for a 5,000-piece run wastes money. When the SKU ends, you walk away with no sunk tooling on the books.
The design can still change
Aluminum and P20 forgive. We can weld or re-cut a soft tool in days. On hardened H13, the same change can mean a new insert and a week of EDM time. If your design is still settling, run a low volume mold first. Lock the geometry on real parts, then cut the production tool once.
Catch the hidden problems early
Short shots near thin ribs, sink behind a boss, flash at a shut-off you thought was sealed. None of this shows in CAD. It shows at T1. Catching it on a soft tool costs far less than on a production tool. If a rib must thicken or a gate must move, you still have room to fix it.
For more cases, read the benefits of short-run plastics and how low volume injection molding helps startups.
Rapid Injection Molding Tooling: Aluminum, P20 or Bridge
For most low volume work, aluminum inserts or P20 cavities beat hardened steel. They machine and polish faster, and cutters last longer on soft metal. You do not need 500,000-shot tool life. You need 5,000 to 50,000.
| Rapid tool | Best fit | Design changes | Watch out for |
|---|---|---|---|
| Aluminum inserts in a master shoe | Under ~1,000 parts, unfilled resins | Weld or re-cut in days | Glass-filled resin and lifters wear it fast |
| P20 single-cavity bridge tool | ~1,000–10,000 parts, side actions needed | Weld or re-cut in days | Slower to cut than aluminum |
| Hardened H13 production tool | 10,000+ parts, glass-filled resins | New insert plus EDM, about a week | Highest cost and longest build |
The 1,000-part line is a rough cutoff. Below it, aluminum is almost always the right call. Between 1,000 and 10,000, the resin decides, since glass-filled nylon eats aluminum faster than ABS. Above 10,000, P20 or H13 starts to pay for itself. No official rule exists. The 1,000 mark is just where the math usually tips.
Before you write aluminum off as prototype-only, read MoldMaking Technology on aluminum tooling myths. For hardened grades, compare them in P20 vs 718H vs H13 vs S136.
- Upfront cost drops, because a small aluminum or P20 tool replaces a multi-cavity hardened mold.
- First parts arrive sooner, with T1 samples in about three weeks on most jobs.
- You mold in the real resin grade, not a print approximation.
- Design changes stay cheap, because soft tools weld and re-cut without major rework.
- A short run slots between bigger jobs without stopping the shop.
Rapid Injection Molding for Prototyping
A prototype mold exists for one reason. It produces a real injected sample of the part, not a perfect one.
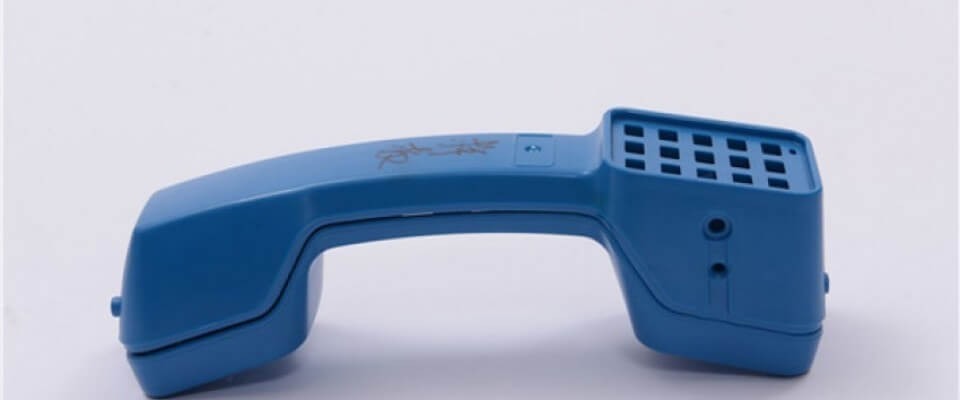
Molded samples tell you things printed samples cannot. Shrinkage, flow lines, sink near thick sections and gate behavior show up only under real injection conditions.
A prototype tool often costs less than a long flow-simulation study, and it hands you a part you can hold. Mold material can be mild steel, aluminum or even epoxy in some cases. Anything that holds geometry under real pressure and melt temperature qualifies.
Cut what you do not need. Drop tight tolerances on non-functional surfaces. Skip polish unless the part is cosmetic. Cooling channels can wait if the part is small and the press can pause between shots.
Ejector pins can sometimes give way to air blow at the parting line. We have shipped working samples this way for small housings under 80 mm. Threads can be molded on loose inserts that come out with the part and get unscrewed by hand.
Loose inserts also replace side-action cores or lifters on a prototype tool. The insert sits in the cavity and the part molds around it. The operator pulls both out together. The cycle runs slower, but the tool costs far less.
If a feature is too detailed to mold, leave it off and machine it afterwards. A drilled hole or milled slot beats a side action you will scrap in two months.
Prototype shops often use a master mold shoe with swappable inserts. One frame serves many cavities. We have had customers run 12 different parts through one shoe in a year. The gate is usually a simple sprue or short edge gate, trimmed by hand after ejection.
The Rapid Injection Molding Process
CAD + quantity → Free DFM → Rapid tool (aluminum or P20) → T1 samples → Short run → Scale or stop
A rapid project moves through the same stages as a production job, only with a smaller tool and shorter loops. Once the tool is on the press, every shot runs the same four-step cycle:
| Step | What happens |
|---|---|
| Clamping | The mold halves close under clamp force before any plastic moves. Tonnage must beat the injection pressure pushing the mold open, or every shot flashes. |
| Injection | Pellets melt in the heated barrel. The screw meters the dose and drives the melt into the cavity at high pressure. |
| Cooling | The melt freezes from the cavity wall inward. Cooling time follows wall thickness, resin and mold temperature, and takes the largest share of the cycle. |
| Ejection | The mold opens and ejector pins push the part out. On a clean tool with good cooling, housing-sized parts cycle in tens of seconds. |

Want a cycle-time estimate for your part? Try our injection molding cycle calculator.
Why Run Low Volume Injection Molding in China
Buyers comparing low volume injection molding in China usually weigh two numbers: piece price and tooling cost. China wins on the second more than the first. Resin costs roughly the same everywhere. The mold does not.
A mold is mostly machining hours, bench work and steel. In China, machining hours and bench work cost far less than in the US or Europe. A single-cavity P20 or aluminum tool that is hard to justify at Western rates becomes an easy decision here. For where the money goes, see this breakdown of Chinese mold costs.
P20 and aluminum plate are stocked in standard sizes by Chinese steel suppliers. A low volume tool starts from plate on the shelf, with no special order and no wait. H13 stays reserved for jobs that need the hardness.
Chinese mold shops commonly run around the clock. A T1 sample in about three weeks is normal for a straightforward part, not a rush surcharge.
Time zones worry first-time buyers more than they should. The fix is process, not geography. One engineer owns your file from quote to shipment. Questions get answered in English with marked-up CAD, not one-line replies.
How to compare low volume injection molding companies
The risk in China is picking the wrong shop, not the country. Check four things before you commit:
- Do they own the presses and the toolroom, or resell someone else’s? See manufacturer vs trading company.
- Do they run aluminum or master-shoe tooling, or quote every job as production steel?
- Will they state tool steel, cavity count and T1 date in the quote?
- Can they move the same part to production tooling when volume grows?
For a wider shortlist, see how China’s top mold makers compare.
Design Tips for Low Volume Parts
A few design choices save real money before we cut steel. Designing for an aluminum mold is not quite the same as designing for H13.
Keep the part simple and avoid lifters and side actions where you can. Aluminum is soft, and repeated lifter action wears it down fast. If a side action is unavoidable, move the tool to P20.
Draft matters more than most buyers expect. Without it, the part drags on ejection. Aim for at least 0.5 degrees on vertical faces, and two to three degrees is better. Textured surfaces need more, sometimes 5 degrees or higher.
Wall thickness is the next big lever. Thicker is not stronger. Thick walls cool unevenly, causing sink outside and stress inside. For most thermoplastics, hold walls between 1.0 mm and 3.5 mm and keep them uniform. Core out a thick boss instead of leaving it solid.
Skip cosmetic polish unless the end user sees the part. A hand-polished SPI A1 finish adds days of bench time. If the part lives inside a housing, SPI B or C works fine. Our surface finish guide shows what each grade means.
For the full checklist, see how our DFM review works, or the 101 tips for low volume injection molding.
From Low Volume to Mass Production
Full hardened tooling earns its keep at hundreds of thousands of identical parts. When you do not need that volume, do not pay for that tool. Bridge tooling and aluminum molds close the gap.
We see this staged approach most with hardware startups, medical device pilots, automotive aftermarket parts and small consumer brands. Prove the design on a soft tool, then scale to production steel. The production tool is covered on our injection mould tooling page, and full-volume runs on our injection moulding in China page.
For the handover in detail, read going from prototype to production and scaling from low volume to mass production.
From design review through final QC, the same project lead stays on your file. Buyers underestimate this. Communication speed matters more than the cheapest quote.
Low Volume Injection Molding FAQs
Fast-quote tip: send 3D and 2D files, target quantity, resin, cosmetic faces, tolerances and inspection needs. That is everything we need to quote without back-and-forth.
How much does low volume injection molding cost?
Simple aluminum or P20 prototype tools start around $1,500. Cost rises with part size, side actions and finish. Per-part price runs higher than on a multi-cavity production tool, but your upfront cash is far lower. Our injection mold cost guide shows what drives the number.
What is the typical lead time for low volume production?
T1 samples typically arrive about three weeks after DFM approval on a straightforward part. Most low volume builds then ship parts 7 to 15 days after mold sign-off. Part complexity, resin availability and tool grade move that window. We confirm a firm date once we have your 3D files and quantities.
What is your MOQ for low volume injection molding?
Typical MOQ is 100 to 500 pieces. The exact number follows part size, resin, cosmetic spec and tooling route. A small ABS housing on a prototype tool can start at the low end. A large glass-filled part on a bridge tool starts higher.
Which is best: prototype, bridge or production tooling?
Pick prototype tooling when the design is still moving. Pick bridge tooling for pilot batches or early sales. Move to production tooling once the design is locked and demand is visible. If you are unsure, send the file and we will recommend one.
Can a low volume mold be used for production later?
Often, yes. A P20 bridge tool can keep running while demand builds. Aluminum suits shorter runs and unfilled resins. When volume outgrows the soft tool, we build a production tool from the same proven design.
What materials can you run for low volume production?
We run most commodity and engineering plastics: ABS, PC, PP, PA6 and PA66, POM, PMMA, PBT and glass-filled blends. Load, temperature, chemical contact, finish and end use decide the grade. Tell us what the part must survive and we will narrow it to two or three options.
Ready to Start Your Low Volume Project?
Holding a CAD file and wondering whether low volume fits your part? Send it over. We will tell you which route fits, and that answer is free.
Get a Free DFM Review & Quote →No drawings yet? Tell us about your part.
