
High-Temperature Plastics
PEEK injection molding turns the most heat-resistant melt-processable plastic into complex parts at production volume. The melt runs at 360–400°C. The mold itself sits at 160–200°C, hotter than the melt point of most commodity resins. Shops without high-temperature barrels, oil-heated tools, and strict drying discipline scrap expensive resin fast. This guide covers the temperatures, grades, tooling rules, and costs that decide whether a PEEK part succeeds.
PEEK (polyether ether ketone) at a glance. Melting point 343°C. Glass transition 143°C. Continuous service temperature up to 250°C. Unfilled tensile strength around 98 MPa. It shrugs off steam, hot water, and most industrial chemicals. That profile is why engineers reach for it when metals feel too heavy and other plastics melt, creep, or dissolve.
What PEEK Is, and Why It Gets Molded
PEEK is a semi-crystalline polymer from the polyaryletherketone family. Victrex commercialised it in the early 1980s. Solvay and Evonik later added their own grades. Four decades on, it still sits near the top of the polymer pyramid.
The material earns that spot with an unusual combination. It keeps stiffness at temperatures that soften PPS or PEI. It resists hydrolysis, so steam sterilisation barely touches it. Almost no common solvent attacks it below 250°C. Wear behaviour is closer to a filled engineering plastic than a neat resin.
None of that matters if the part shape fights the budget. Machining PEEK from rod or plate wastes most of a very expensive blank. Injection molding flips the maths once volume arrives. The tool costs real money, yet each shot uses grams of resin instead of a machined billet. Complex geometry comes out of the mold net-shape, threads, bosses, and clips included.
The catch is process discipline. PEEK punishes shortcuts that ABS would forgive. Wet resin degrades in the barrel. A cold mold leaves an amorphous skin that turns brittle. Undersized gates shear-thin the melt and starve thick sections. Every section below traces back to one of those failure modes.
PEEK Injection Molding Temperatures
Temperature control is the whole game with this resin. The window below reflects standard practice for unfilled grades such as Victrex 450G. Filled grades run a few degrees hotter at the nozzle.
| Parameter | Typical Setting | Why It Matters |
|---|---|---|
| Drying | 150°C for 3 hours, to under 0.02% moisture | Wet PEEK hydrolyses at melt temperature and loses molecular weight |
| Barrel, rear zone | 350–360°C | Feeds pellets without bridging or premature melting |
| Barrel, middle zones | 365–385°C | Builds a fully molten, uniform melt |
| Barrel, front zone and nozzle | 380–400°C | Keeps viscosity low enough to fill thin walls |
| Mold temperature | 160–200°C | Drives crystallinity, which sets strength and chemical resistance |
| Ejection temperature | Below 200°C part temperature | PEEK stays rigid enough to eject without distortion |
The mold temperature row deserves a second look. Below roughly 160°C, the surface freezes before crystals form. Parts come out with a brownish, translucent skin. That skin signals an amorphous layer with weaker chemical resistance and lower fatigue life. We see this defect on samples from shops that ran PEEK in a water-heated tool. Water controllers top out near 140°C under pressure. They simply cannot hold a PEEK mold at temperature.
Crystallinity is measurable, not a matter of opinion. A DSC scan on a first-article part shows the crystallisation peak clearly. Ask any PEEK molder for that scan. A shop that cannot produce one is guessing at its own process.
PEEK Grades Buyers Actually Specify
Grade choice drives shrinkage, wear, and price more than any machine setting. These are the grades that appear on drawings again and again.
| Grade Type | Common Examples | Shrinkage (flow direction) | Typical Use |
|---|---|---|---|
| Unfilled | Victrex 450G, KetaSpire KT-820 | 1.0–1.5% | General high-temperature parts, insulators |
| 30% glass filled | Victrex 450GL30 | 0.3–0.6% | Structural brackets, pump components |
| 30% carbon filled | Victrex 450CA30 | 0.2–0.5% | Stiff, conductive, wear-resistant parts |
| Bearing grade | Victrex 450FC30 | 0.3–0.6% | Bushings, seals, thrust washers |
Filled grades shrink less along the flow and more across it. That anisotropy warps flat parts if the gate sits in the wrong place. We cover the tooling response in the mold design section below.
Chinese domestic PEEK has improved fast. Producers such as Junhua sell unfilled grades well below Victrex pricing. Batch consistency still varies more than the European brands. For brackets and housings, domestic resin often passes every test. For aerospace or implant-adjacent work, most buyers stay with Victrex or Solvay and demand lot certificates. Decide by test data, not by flag.
One grade boundary matters commercially. Medical implant-grade PEEK is a separate supply chain with its own pricing and paperwork. Standard industrial grades, even medical-device grades, do not cross into implant use. If your part touches the body permanently, say so in the RFQ.
Equipment That Separates Real PEEK Shops
A standard press tops out around 300°C at the barrel. PEEK needs 400°C capability with stable control at that ceiling. Ask a supplier one question early. What is the maximum barrel temperature on the machine booked for your job? A vague answer ends the audit.
The mold heating system matters just as much. Oil circulation units and electric cartridge systems hold 160–200°C all shift. They cost more to run than water units. Some shops quote PEEK work, then quietly run the tool cold to save the heating bill. The parts tell on them within one DSC scan.
Filled grades add a wear problem. Glass and carbon fibres chew through standard screws, barrels, and non-return valves. Production PEEK work needs hardened or bimetallic barrel sets. Worn components show up as black specks and inconsistent shot weight. If a shop runs GL30 daily on a general-purpose screw, ask how often they rebuild it.
Drying kit completes the picture. A desiccant dryer with a dew point near −40°C, plus sealed conveying to the hopper. Open gaylords next to the press undo four hours of drying in one humid afternoon. Walk the floor during any audit and look at the hopper first.
Mold Design Rules for PEEK
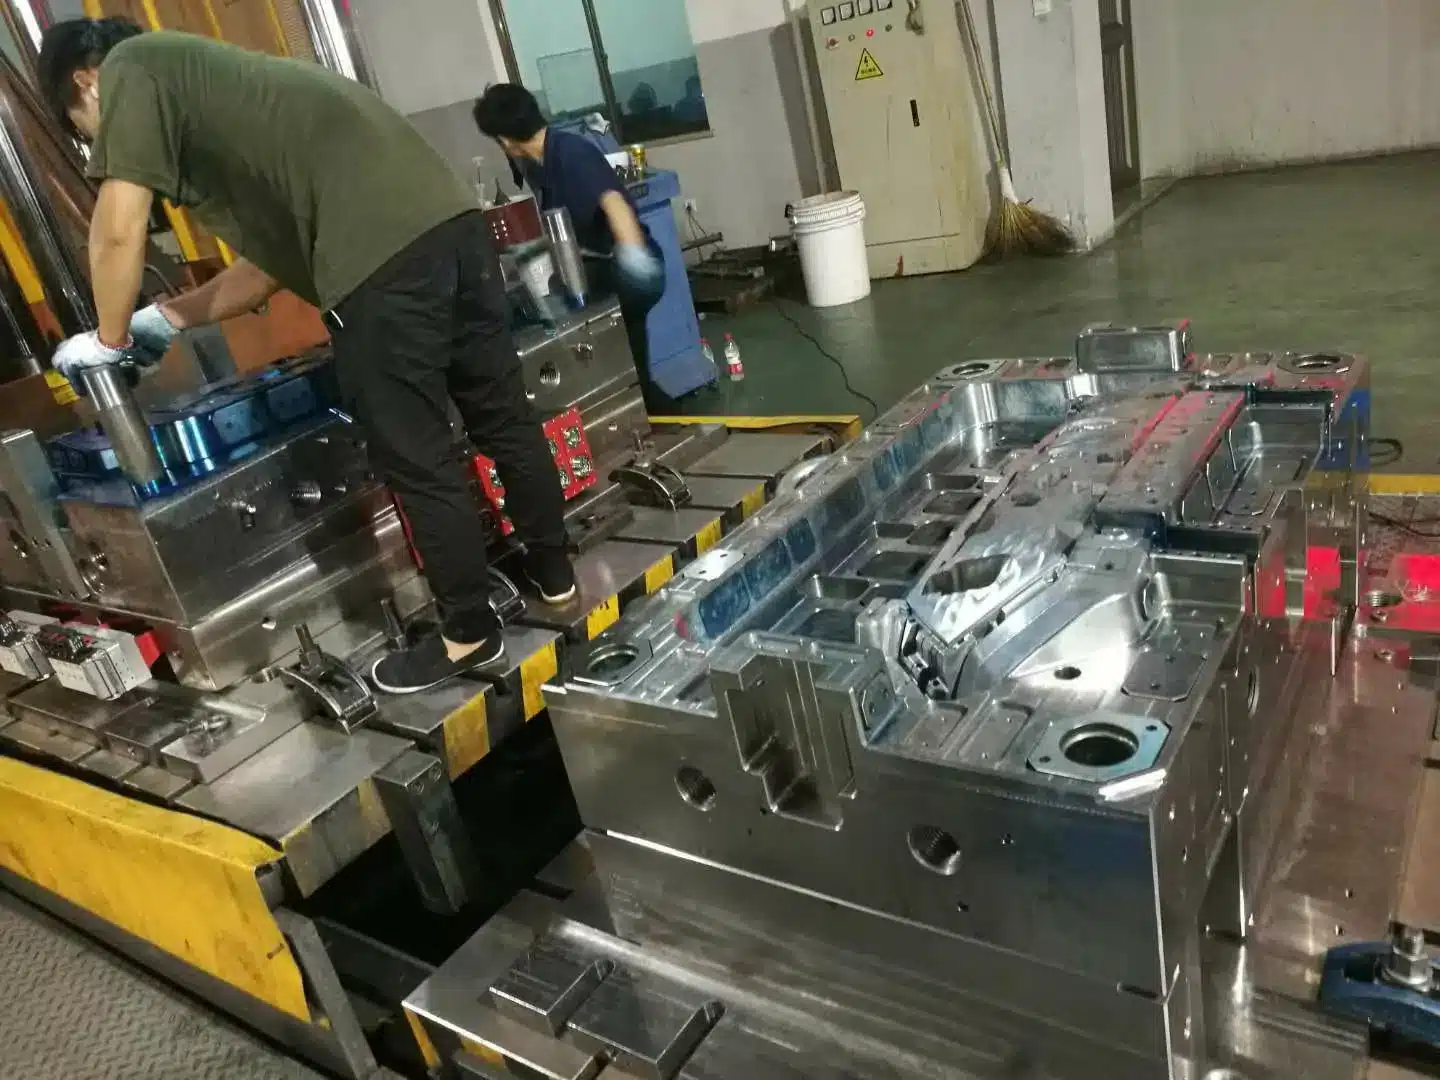
PEEK tooling starts with steel. Production molds run hardened H13 or S136 at roughly 48–52 HRC. Soft P20 might survive unfilled resin trials. Glass-filled grades will wash out its gates within a short production run. Gate erosion changes fill balance, and the part drifts out of tolerance slowly enough to miss.
Gates run larger than buyers expect. PEEK melt is viscous, and pressure drop across a small gate starves the cavity. Pin gates that work beautifully in PC leave short shots and weak weld lines here. Edge and tab gates suit most geometries. Direct sprue gates suit thick, simple parts. Our interactive tooling pages show how gate choice moves cost and quality.
Runners split the field. Cold runners waste costly resin on every shot, although the scrap stays visible and countable. Hot runners save material but hold PEEK at 380°C for hours. Long residence degrades the polymer and shows as dark streaks. For short runs and frequent grade changes, we favour cold runners. For stable, high-volume programs, a well-designed hot runner pays back.
Venting needs care at these temperatures. Vents run shallower than commodity-resin practice, around 0.01–0.02 mm on the land. Deeper vents flash because the melt finds them before it freezes. Cooling design also differs. The tool must hold temperature evenly, so heater layout and insulation plates matter more than raw water flow. A mold that swings 15°C across its face prints that swing into the part as warpage.
Part Design Rules That Keep PEEK Moldable
Most PEEK parts sit between 1 mm and 4 mm wall. Thinner walls fill, but the pressure needed climbs steeply. Thicker sections cool slowly and hide voids at the core. A void inside a sealing face fails in service, not on the inspection bench. Keep walls uniform and core out heavy bosses instead of leaving solid blocks.
Sharp internal corners concentrate stress in a stiff, notch-sensitive material. Give internal radii at least 0.5 mm where the design allows. External corners can stay sharper. Draft of 1° per side releases most surfaces cleanly. Polished or textured faces need more, the same as any resin.
Ribs follow the usual proportions, roughly 60% of the adjoining wall thickness. With PEEK the temptation is to oversize ribs because the material feels premium. Oversized ribs print sink marks on the show face and trap gas at the rib root. A design for manufacturability review catches these before steel is cut. On PEEK, that timing matters. Steel changes cost more when the tool is hardened and built for 200°C service.
Threads deserve a mention. Molded internal threads in PEEK work, but coarse profiles survive better than fine ones. Fine threads in filled grades chip at ejection. Many buyers mold a plain bore and tap it later. That hybrid route often beats forcing the mold to do everything.
Tolerances and Shrinkage Control
PEEK rewards a toolmaker who cuts steel to measured shrinkage, not datasheet shrinkage. Unfilled grades shrink 1.0–1.5% depending on wall and process. Filled grades shrink less along flow and nearly double across it. First-article measurement on a trial tool settles the real numbers for your geometry.
On achievable tolerance, be precise about the claim. ±0.05 mm is realistic on short, stable dimensions with a controlled process. It is not realistic across a 200 mm span in a glass-filled grade. Temperature swings in service move PEEK less than most plastics, which helps. Anisotropy hurts more than thermal expansion at these sizes.
Crystallinity links back into dimensions. A part molded at 170°C and one molded at 195°C leave the same tool with different crystal content. Their dimensions drift apart during any later heat exposure. Lock the mold temperature in the process sheet. Treat it as a dimension, not a preference. Buyers comparing quotes should ask each shop what mold temperature its price assumes.
Injection Molding vs. Machining vs. Compression Molding
Three processes compete for PEEK parts, and the honest answer depends on volume and tolerance. Machining wins prototypes and tiny batches. No tooling bill arrives, and tolerances on turned features beat molding. The blank waste is the tax. A machined seal can consume five times its finished weight in rod stock.
Compression molding suits large, simple shapes and stock shapes for later machining. Cycle times run long and geometry stays basic. It rarely competes for small, detailed components. Injection molding takes over once annual volume reaches the low thousands. Tooling amortises, cycle times drop under a minute, and detail comes free.
| Factor | Injection Molding | CNC Machining | Compression Molding |
|---|---|---|---|
| Best volume | Thousands and up | Ones to hundreds | Hundreds, simple shapes |
| Geometry | Complex, net-shape | Limited by tool access | Basic, flat or gently curved |
| Material waste | Low, runner scrap only | High, blank becomes chips | Low to moderate |
| Tightest tolerance | ±0.05 mm on stable features | ±0.01 mm possible | Moderate |
| Upfront cost | Hardened production tool | Programming and fixtures | Simpler tool, long cycles |
A hybrid path serves many programs well. Machine the first fifty parts from stock shapes while the mold is being cut. Validate the design in real PEEK. Then switch to molding for production and keep machining for service spares. The resin bill for those fifty parts hurts less than re-cutting a hardened tool twice.
What PEEK Injection Molding Costs
Resin dominates the part price. Standard unfilled grades start near $100 per kg. Victrex 450G commonly trades at $120–150 per kg in 25 kg lots. That is roughly twenty times the price of ABS. A 40-gram part carries $5 of polymer before the press even cycles. Runner scrap, drying losses, and start-up purges add their share on top.
Tooling costs more than commodity work for three reasons. The steel is hardened and finished to a higher grade. Heaters, insulation, and temperature control hardware add components. And the trial process takes longer, because every parameter change needs a stabilised tool at 180°C. Buyers comparing a PEEK quote against a PC quote for the same geometry should expect a clear gap.
Volume bends the curve hard. At 500 parts, tooling is most of the program cost and machining usually wins. At 50,000 parts, resin is almost the whole story and the press rate fades into noise. The crossover for typical small components sits somewhere in the low thousands. Run both numbers before committing. A structured injection molding RFQ template forces every bidder onto the same scope, which makes the comparison honest.
China changes the tooling side of the equation most. Labour and machining rates put a hardened PEEK tool well below US or EU pricing. The resin, bought from the same global makers, costs about the same everywhere. So the China advantage concentrates in tooling and conversion, not material. That is also where audit effort belongs.
Defects We Watch for on First PEEK Parts
Short shots arrive first when anything is off. Cold melt, a cold mold, or an undersized gate all produce them. The fix differs each time, so changing two variables at once wastes a trial day.
Brittle parts point at crystallinity. The part looks complete, then snaps at a load commodity plastic would survive. Check the mold temperature record before blaming the resin lot. Nine times out of ten the tool ran cold.
Weld lines weaken PEEK more than most materials. The melt fronts meet at high viscosity and knit poorly. Gate relocation beats parameter tweaking here. Moving a gate costs steel time once. Living with a weak weld line costs field failures forever.
Voids hide inside thick sections. Surface quality gives no warning. Section the first article, or scan it, before approving the tool. Dark streaks and specks trace back to degraded resin or a worn barrel. Both signal process neglect that will grow worse across a production run, not better.
How to Vet a PEEK Injection Molding Manufacturer
Five checks filter the field quickly. First, barrel capability on the actual booked machine, stated in degrees. Second, the mold heating method, oil or electric, with its working range. Third, drying equipment and the dew point it holds. Fourth, whether first-article approval includes DSC crystallinity data. Fifth, resin sourcing, with lot certificates available for the grade on your drawing.
Ask about steel and wear practice too. A serious PEEK shop answers with grades and hardness numbers, not adjectives. Our own tools follow the same logic we apply across PPS injection molding and other high-temperature work. The disciplines overlap heavily. Drying discipline, hardened steel, and measured shrinkage decide outcomes in both materials.
Certification questions need precision. ISO 9001 covers the quality system, and its requirements sit on the ISO website. It does not certify the part in your hand. For regulated work, ask which standards the shop has actually shipped against. Then request the inspection records from one such job, redacted if needed. Shops with the experience produce them in a day.
Resin makers publish their own processing guides, and the Victrex site is the reference most engineers start from. Compare any supplier’s stated window against that baseline. A shop claiming success at a 280°C melt is describing a different polymer, or a short career for your parts.
Where Molded PEEK Parts Earn Their Price
Aerospace uses PEEK for brackets, clips, and electrical housings that must survive heat and vibration. Weight saved against aluminium compounds across a fleet. Semiconductor fabs specify it for wafer handling and CMP retainer rings. The material resists the process chemicals and sheds few particles when grades are chosen well.
Medical work splits into two camps. Sterilisable instrument handles, housings, and trays use industrial or medical-device grades. They endure thousands of autoclave cycles without cracking. Implant components sit under separate rules and resin grades, as noted earlier.
Oil and gas runs PEEK seals, backup rings, and valve seats at pressure and temperature together. Automotive and EV programs use it in transmission wear parts, pump gears, and high-voltage connectors. In each case the buyer pays for survival, not appearance. Nobody chooses this resin for a part that lives an easy life.
Frequently Asked Questions
Can PEEK be injection molded on a standard machine?
Usually not. Standard barrels rarely exceed 300°C, while PEEK melts need 360–400°C. The mold also needs heating to 160–200°C, beyond water-based controllers. A capable machine has high-temperature barrel heaters, insulation, and an oil or electric mold temperature unit. Ask for those specifications in writing before placing an order.
What temperatures does PEEK injection molding need?
Dry the resin at 150°C for about three hours, down to under 0.02% moisture. Run the barrel from 350°C at the rear to 380–400°C at the nozzle. Hold the mold between 160 and 200°C. That mold temperature sets crystallinity. Running colder produces an amorphous skin and brittle parts.
How much does PEEK resin cost?
Standard unfilled grades start near $100 per kg. Victrex 450G commonly trades around $120–150 per kg in 25 kg lots. Filled and specialty grades cost more. Chinese domestic grades cost less, with wider batch variation. Resin usually dominates the finished part price, so grade selection is a commercial decision too.
What shrinkage should a PEEK mold allow for?
Unfilled PEEK shrinks about 1.0–1.5%, depending on wall thickness and process settings. Glass-filled grades shrink 0.3–0.6% along the flow direction and more across it. Carbon-filled grades sit slightly lower again. Cut the tool steel-safe where possible. Then correct dimensions from first-article measurements on your actual geometry.
Should I machine or injection mold my PEEK part?
Machine prototypes and batches in the hundreds. There is no tooling bill, and tolerances run tighter. Injection mold once annual volume reaches the low thousands. The tool pays back through low waste and short cycles. Many programs machine early parts from stock shapes, then move to molding for production without changing material.
How long does a PEEK mold last?
Steel choice decides the answer. Hardened H13 or S136 at 48–52 HRC handles filled grades and long production runs. Soft steel wears at the gates, especially with glass-filled resin, and dimensions drift. A hardened, maintained tool normally outlasts the product lifecycle. Gate condition is the first wear point to inspect at each service.
What lead time is realistic for a PEEK molding program?
Tooling for a hardened PEEK mold typically takes four to eight weeks, depending on complexity. First samples follow within about a week of tool completion. Resin procurement can add time for less common grades. Confirm the exact grade and lot early, because a missing resin certificate stops shipment faster than any machine problem.
Send us your PEEK drawing or 3D file. We reply with a DFM review, a steel and grade recommendation, and a quote that separates tooling from part price. Get a Free DFM Review

