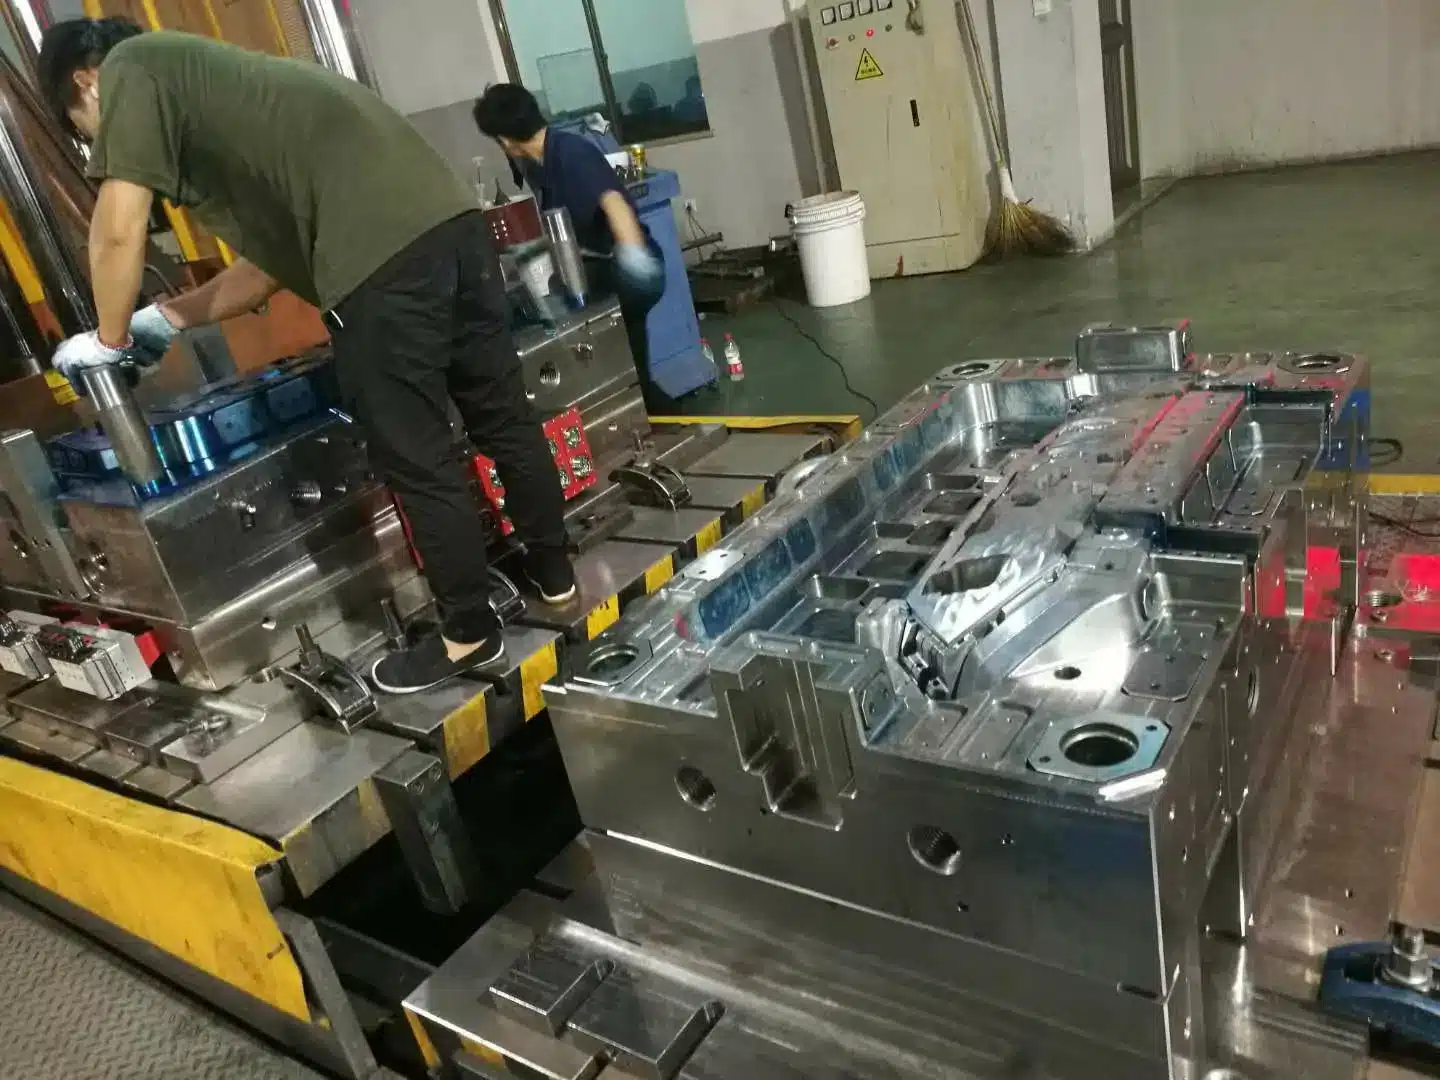

Toolroom & Press Setup
21 Plastic Mold Building and Setup Tips from Senior Toolmakers
Building a reliable plastic mold that runs flash-free and holds cycle time requires strict shop-floor discipline across parting-line venting, dual-zone thermal control, clamp rigging, and preventative maintenance.
- Parting Line Venting: Cut at least 6 vents on small molds and cover at least 30% of the parting line perimeter on production tools; clean vents every 24 hours.
- Mold Half Temperature Delta: Run separate TCUs for core and cavity; keep surface variance within 5–10°F and run the ejection half 5 to 12°F hotter so parts stay on the ejector side.
- Waterline Scale Loss: Descale cooling channels monthly; just 1/64 in. of mineral scale inside a 1/4 in. waterline destroys 40% of cooling efficiency.
- Annual Maintenance Budget: Preventative mold maintenance typically costs 5% to 7% of initial tooling investment per year.
Apply these 21 proven toolmaking and press-setup rules to prevent trapped gas burns, cooling hot spots, platen clamp slip, and cavity steel scratches:
| Tooling System | Shop-Floor Specification | Engineering Purpose |
|---|---|---|
| Parting Line Vents | Min. 6 vents (small molds) or ≥30% of parting perimeter | Prevents diesel burn marks and short shots; clean every 24 hours |
| Temporary Shut-Off Vent | Two strips of 1/2 in. masking tape with a 1/2 in. gap | Tests whether trapped gas is causing a short shot in 1–2 trial shots |
| Pyrometer Surface Check | Max 10°F spread across 5–6 points (5°F on critical faces) | Detects blocked cooling channels or laminar water flow |
| Ejection vs. Injection Half | Heat ejection half 5°F to 12°F warmer than stationary half | Ensures part shrinks onto ejector core without thermal lock-up/galling |
| Toe Clamp Heel Shim | Place a 1/8 in. metal washer under clamp heel | Angles clamp toe 1/8 in. toward platen so thermal expansion cannot slip mold |
| Waterline Descaling | Descale monthly (1/64 in. scale = 40% cooling loss) | Restores turbulent heat transfer inside 1/4 in. drilled lines |
Parting Line Venting & Mold Temperature Control (Tips 1–11)
1. Small injection molds require a minimum of 6 parting line vents, while larger molds require vents distributed around the entire cavity perimeter leading out to open atmosphere. Clean vent lands at least once every 24 hours. As a shop-floor rule of thumb, venting should cover at least 30% of the parting line perimeter—provided vent depth stays below the resin flash threshold.

2. To verify whether an unvented shut-off is causing a gas trap during T1 trials, apply two strips of 1/2 in. wide masking tape on the shut-off face with a 1/2 in. gap between them, then shoot one or two test cycles to see if the burn mark or knit line disappears.
3. Never loop both mold halves through a single temperature control unit (TCU). Control the stationary cavity half and moving core half on separate TCUs so each side holds its target temperature independently and the molded part reliably stays on the ejection half.
4. Plumb mold cooling manifolds so cooling water enters near the bottom of the mold block and exits near the top. Bottom-to-top flow purges trapped air pockets out of the waterlines immediately, preventing localized steam pockets and hot spots.
5. Measure actual steel cavity temperature periodically using a flat-probed surface pyrometer across 5 to 6 spots on each mold half. Temperature variance between any two points or between mold halves must not exceed 10°F. If the spread exceeds 10°F, descale the channels, add cooling lines, or install internal baffles.
6. Thermoplastics naturally cling to the hotter mold half as they shrink. Keeping the moving clamp/ejection side slightly warmer prevents the part from sticking in the stationary cavity half and reduces demolding warpage.

7. Set the ejection half of the mold 5°F to 12°F warmer than the stationary injection half to keep parts on the core. Never exceed a 12°F differential on tight-fitting steel, as excessive thermal expansion mismatch causes guide-pin lock-up or sliding metal galling.
8. Running a hotter mold surface produces higher part gloss and deeper, slightly darker pigment appearance compared to running a cold mold.
9. Bolt commercial thermal insulation boards (available in 1/4 in. and 1/2 in. thicknesses) directly to the back of the mold clamp plates to stop conductive heat loss into the press platens and keep cavity temperatures uniform.
10. Feel the outgoing supply hose and returning drain hose on the TCU by hand. If the return line feels substantially hotter than the supply line, the mold is generating more heat than the flow rate can remove—indicating restricted flow or undersized pumping capacity.
11. Descale mold waterlines at least once a month. A mineral scale layer just 1/64 in. thick inside a 1/4 in. waterline cuts cooling heat-transfer efficiency by 40%.
Clamp Rigging, Brass Purge Tools & Gating (Tips 12–21)
12. Place a 1/8 in. metal shim (washer) under the rear heel of each toe clamp when mounting a mold in the press. Tilting the clamp toe slightly (1/8 in.) toward the platen directs clamping force inward against the platen face; perfectly parallel clamps can slip loose as the mold and tie-bars expand and contract thermally.

13. Install right-angle hose fittings at the mold manifold inlets to trip turbulent water flow inside straight drilled channels. Verify thermal uniformity by taking at least 3 pyrometer readings across the melt-contact face; the three readings should stay within 5°F of each other.
14. Never report the TCU controller digital setpoint when asked for the mold temperature. Always measure and log the actual steel surface temperature on the cavity face using a calibrated pyrometer.
15. Never use steel screwdrivers, pliers, or picks to pry stuck plastic out of a cavity or sprue bushing. Steel tools scratch polished tool steel; equip every press exclusively with soft brass bars, wood dowels, and copper or plastic wedges.
16. To extract a broken sprue wedged inside a sprue bushing, heat a brass wood screw, thread it into the center of the plastic sprue, let the resin solidify, and pull the screw head out using brass pliers.
17. To clear stuck plastic from deep, narrow rib slots, heat a copper or brass hacksaw blade and melt it into the stuck rib so it pulls out cleanly without scoring the steel walls.
18. Position the injection gate at the thickest wall section of the part. Injecting from thick to thin builds uniform flow resistance and allows packing pressure to compress the melt completely before thin sections freeze off.
19. While the customer owns the capital mold asset, the injection molder is responsible for routine preventive maintenance in the press. Annual mold maintenance budgets typically run between 5% and 7% of the initial mold build cost.
20. At the end of a production run, purge all cooling waterlines completely with compressed air to prevent internal rust and mineral deposition before removing the mold from the press.
21. Spray the cleaned cavity and core surfaces with a protective rust preventative,and store the **last molded shot** inside the tool box alongside the mold so the toolroom has a physical reference sample before the next production run.
Looking for a custom mold maker that builds long-life export tooling with full DFM and maintenance documentation? Send us your part files today.

