
Robotics & AI Hardware
Robots and AI servers run on molded plastic parts, from exterior shells to connector insulators and fan shrouds. This page collects our engineering guides for those parts, grouped by the decision each one settles. Volumes are still low, designs still move, and the wrong tooling call costs quarters.
Market and material decisions
Humanoid programs live at bridge-tool volumes today. Tool the parts that will not change, machine the rest, and expect the split to move every quarter.
Our guide to plastic parts for humanoid robots works through the tooling math, part by part.
Resin choice kills more robot parts than bad molding does. The robot plastic material selection guide ranks each resin against continuous temperature first, then load, moisture exposure, and cost per part.
Parts and processes
Four topics come up on nearly every robot program.
A gripper needs a hard skeleton and a soft face in one part. 2K and LSR molding for robot hands covers the pairs that bond, and the peel failures that follow a wrong pairing.
POM stays the default resin for molded robot gears. The robot plastic gears guide covers gate placement, shrink compensation, and the joints where plastic should stay out.
Threads, bearing seats, and electrical contacts all point to one process. Our insert molding for robotics guide covers insert grip, boss design, and the stress cracks that follow sharp corners.
Connectors get the longest section on this page, because the tolerances leave no room to improvise.
High-Precision Connector Molding for AI Hardware
AI compute runs on high-speed connectors. Their insulators are injection molded in LCP at tolerances measured in microns, because at 224 Gb/s the plastic itself shapes the signal.
This section covers the resin that dominates high-speed connectors, and the molding problems a multi-pin connector throws at you.
High-speed connector molding in brief:
- Lead resin: LCP (liquid crystal polymer), low warpage, thin wall, strong dielectric properties.
- Tolerance: connector insulators demand micron-level precision and very low shrinkage.
- Signal integrity: a low dielectric constant preserves the signal at high frequency.
- Process: insert molding places terminals precisely; multi-pin parts need flow simulation.
Why LCP dominates high-speed connectors
LCP is the number-one material for board-to-board connectors that move high-speed data. It earns that place on four properties that a connector needs at once.
- Low warpage. A very low thermal expansion means minimal warp, so insulators hold tolerance.
- Thin wall. LCP fills extremely thin sections, down to a few thousandths of an inch, for dense, miniature parts.
- Dielectric performance. Low dielectric constant and dissipation factor at high frequency protect signal integrity.
- Inherent flame rating. LCP hits UL 94V-0 without additives, and runs continuously near 240 °C.
Why it matters at 224G: next-generation connectors support 224 Gb/s-PAM4. At those speeds the insulator's dielectric behavior is part of the electrical design. The resin is not just a holder — it shapes the signal path.
LCP is a material of its own
LCP is semi-crystalline, but it does not behave like other semi-crystalline resins. With most engineering plastics, a molder can pack the cavity harder for a slightly bigger dimension, or adjust cycle to shift shrink.
LCP gives no room to "process around" a problem. You cannot pack or cycle your way out of a dimensional miss the way you can with nylon or PBT. The tool has to be right, and the process has to be dialed. That is why LCP molding is a specialist's job, not a general-purpose one.
Resin shortlist for connectors
| Resin | Strength | Trade-off |
|---|---|---|
| LCP | Thinnest walls, lowest warpage, best high-frequency dielectric | Premium price; unforgiving process |
| PPS | Excellent insulation, high-temp, chemical resistance, dimensional stability | Less extreme thin-wall capability than LCP |
| Glass/mineral-filled PBT, PA | Cost-effective, tight-tolerance capable | Higher dielectric loss than LCP at high frequency |
The molding challenges of a multi-pin connector
A connector body looks small, but it is one of the harder parts to mold well, and the reasons stack up.
- High-viscosity resin, narrow window. The materials are viscous and sensitive to temperature, with a tight processing range.
- Cooling imbalance. The multi-pin structure cools unevenly, which drives sink marks, residual stress, and warpage.
- Weld lines. Flow around pins forms weld lines that cost strength, so they must be placed with care.
- Fast fill. Thin walls must be filled very fast, which demands specialized machines and accurate tooling.
Simulate before you cut steel. For tight-tolerance multi-pin connectors, flow simulation at the design stage tunes gate and cooling layout. It reduces warpage and sink before the tool exists. That beats fixing steel later.
Insert molding for terminal precision
High-speed connectors increasingly use insert molding to place terminals. Molding the plastic around staggered pins holds the position and tolerance that fast signaling needs. It is how leading designs reach higher density and speed. See how insert molding places metal precisely →
Molding a high-speed connector or insulator?
Send your connector drawing and signal spec. We will advise LCP or PPS, run flow simulation, and quote a tool built for micron tolerance.
Send your connector drawing and signal spec.
Frequently asked questions
What plastic is used for high-speed connectors?
LCP (liquid crystal polymer) is the leading choice. It offers low warpage, thin-wall molding, and strong high-frequency dielectric properties. PPS and filled PBT or nylon serve less demanding connectors.
Why is LCP hard to mold?
LCP is viscous and temperature-sensitive. It gives almost no room to adjust dimensions through packing or cycle changes. The tool and process must be right from the start, which makes it a specialist job.
How tight are connector molding tolerances?
Connector insulators demand micron-level precision and very low, consistent shrinkage. LCP's low thermal expansion helps hold those tolerances across a production run.
Why does the plastic affect connector signal quality?
At high data rates, the insulator's dielectric constant and dissipation factor influence the signal. A low-loss resin like LCP preserves signal integrity, so the material is part of the electrical design.
Why use flow simulation for connectors?
Multi-pin connectors cool unevenly, which drives warpage, sink marks, and stress. Simulation tunes gate and cooling layout before the tool is cut. Fewer defects follow, and less steel gets reworked.
Electronics and the rack
Motor drivers make a robot a walking source of interference. The EMI/RFI shielding and ESD guide covers filler choice and the resin-skin trap at every joint.
The same molding logic fills the server rack. Our data center plastic parts guide maps the molded chassis and cooling parts inside a rack, and the flame-retardant resins they run.
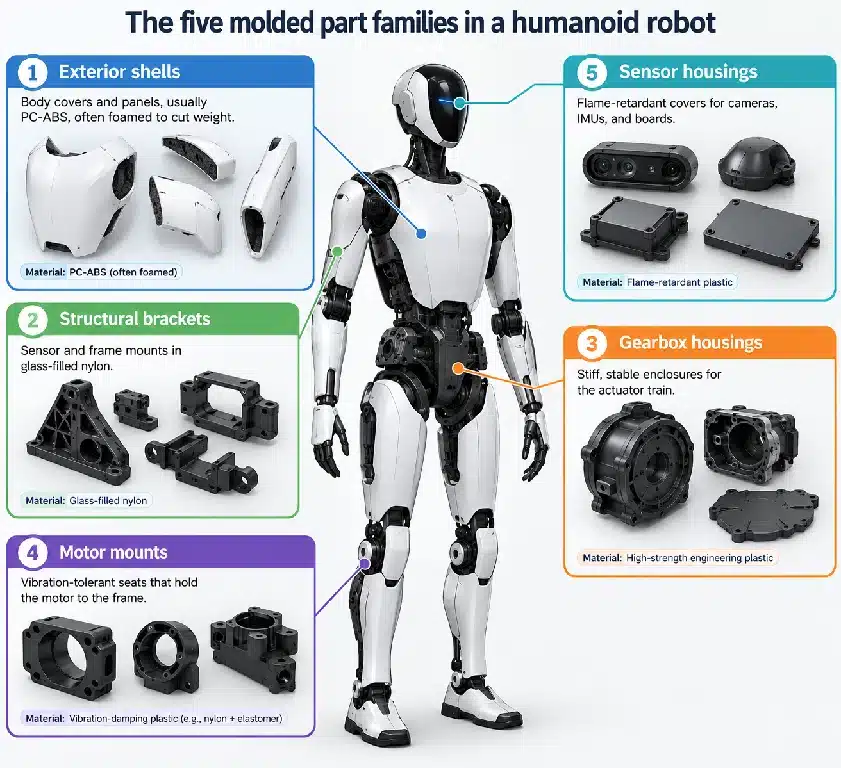
Two service pages turn these guides into a quoted program. The humanoid robot injection molded parts page walks the five part families on a humanoid build. Our robotics and AI hardware injection molding service page covers the part range we mold. It also sets out materials and tooling by project stage.
Send a drawing or STEP file, and we will say plainly what molds well and what should stay machined.

