
Guia de Abastecimento na China
How to Choose China Injection Molding Suppliers in 2026
To choose China injection molding suppliers, check real mold capability, quote honesty, QC records and T1 behavior before you pay for steel. That covers the whole path from inquiry and risk control to sampling, mold building, delivery and stable mass production.
Finding a China injection molding supplier takes ten minutes on Alibaba. Finding one that fits your part, your tolerances and your volume is the hard part. China has dominated injection molding manufacturing for the past ten years, so a long list of names is never the problem.
This guide draws on supply chain management, mold making specifications and years of procurement work inside the industry.
After reading it, you should be able to:
- Tell a capable supplier from a weak one
- Spot whether a quote is genuine or a low-price hook
- Pick the right type of supplier for your product and your volume
- Avoid the usual failures around molds, materials and mass production
- Audit suppliers against a fixed checklist using ready-made templates
- Build a Chinese injection molding supplier selection system your team can reuse
Parte 1 — Por que razão é tão difícil escolher o fornecedor certo de moldagem por injeção na China
Picking a China-based molding supplier looks simple on paper. Compare prices, check a few samples, ask a friend, browse Alibaba, place the order.
It rarely goes that way.
Supplier choice decides success rate, yield, delivery time and final profit more than any other step in the project. This part explains why buyers keep landing in the same traps and why established suppliers still fail. It also covers the low-price trap and why overseas buyers, more than local ones, misjudge how hard a part is to mold.
1. Common Pain Points When Sourcing From Chinese Injection Molding Suppliers
You have probably hit at least one of these already.
1.1 You never see the factory’s real capability
Very few Chinese molding factories will say any of this to a new customer:
- “We don’t have experience with parts at your level”
- “Our mold capability isn’t enough for this”
- “We quoted low because we didn’t understand your accuracy requirement”
- “Nunca fabricámos peças transparentes de qualidade médica”
- “We cannot hold ±0.02mm”
What you hear instead is this.
“Conseguimos. Não há problema. É muito fácil.”
The reasons are cultural as much as commercial. In many Chinese factories:
- Turning a customer away feels like failure
- Losing the order is the bigger fear
- Confidence slides into blind optimism
- People assume the problem can be solved later, once the mold exists
- Nobody has actually pinned down what the customer needs
So the first round of emails tells you almost nothing about whether the factory understands your part.
1.2 Overseas buyers can’t see the real difference in mold quality
Many foreign buyers assume a mold is a mold.
It isn’t. Grade drives lifespan and accuracy, and price follows, as this comparison for an molde de injeção shows. The L1–L4 labels here are working shorthand. The Associação da Indústria dos Plásticos publishes its own formal mold classes.
| Grau de bolor | Candidatura | Vida (tomas) | Exatidão | Diferença de preço |
|---|---|---|---|---|
| L1 | Simple housings, toys | <50 mil | Baixa | Barato |
| L2 | Peças industriais, bens de consumo em geral | 100 mil–300 mil | Médio | Médio |
| L3 | Peças para automóveis, peças estruturais | >500 mil | Elevado | Elevado |
| L4 | Medical, transparent parts, precision parts | >1M | Muito elevado | Muito elevado |
Most failures in this table happen in one spot. The buyer needed L3 and the factory built L1. Nobody explained the difference, and sometimes the factory didn’t know it either.
You thought you got a great deal. What you actually bought was a cheap mold that won’t last.
1.3 The factory won’t tell you the part is hard to make
To you it’s a simple plastic part. The engineer looking at your file may be thinking something else:
- “These undercuts and side holes need sliders or lifters.”
- “This wall is too thin to fill.”
- “That thick section will warp unless we add cooling lines.”
- “We can’t hold this tolerance.”
- “The design itself has a defect.”
They rarely say it out loud. Some worry you’ll place the order elsewhere. Some assume they’ll fix it after T1. Some genuinely don’t see the difficulty, and that is the most dangerous case.
Eventually you get one or more of these:
- No usable sample
- Samples that come back full of problems
- High NG rates
- Parts that won’t assemble
- Real cost 2–3 times higher than the quote
1.4 The low-price trap brings delays and quality failures
This is the trap foreign buyers fall into most often. One quote comes in 30–50% below the others, and it feels like a win. In practice the factory can’t build a good mold on that budget. So it switches to lower-grade steel and cheaper plastic.
Then the bills arrive in a different form:
- Mold life ends up at 1/5 of the quoted figure
- Batch failure rates run 10–40%
- Cycles are slow because the cooling design is poor
- The mold gets modified every month
- Every production run needs rework
- The project never settles down
The lowest offer is often the most expensive one.
1.5 Remote communication keeps causing misunderstandings
Chinese molding factories handle CAD drawings, standard processing requirements and simple structures well. Overseas requirements often go further:
- Normas internacionais de ensaio
- Certificação UL
- Resistência aos raios UV
- Acumulação de tolerâncias de montagem
- Structural room for future product versions
- Supply chain risk and the end user’s experience
These items almost always get skipped in the first round. The usual chain looks like this.
Wrong design → part revision → mold modification → 1–4 months of delay
Or the product simply never reaches its original standard.
1.6 The real situation shows up months later
Nearly every buyer has lived through some version of this timeline:
- Mês 1: Está tudo bem
- Mês 2: A amostra apresenta um pequeno problema
- Mês 3: “Já tens o teu problema de design.”
Halfway through the project, you start learning things nobody mentioned at the start:
- The presses are outdated.
- There aren’t enough technicians.
- You are not a priority customer.
- The shop is overloaded with low-priced orders.
- There is no professional project manager.
- Nobody really understands your parts.
- Your part has been quietly subcontracted to another plant.
By then it is too late to change factories.
2. Match the Factory Type to Your Part
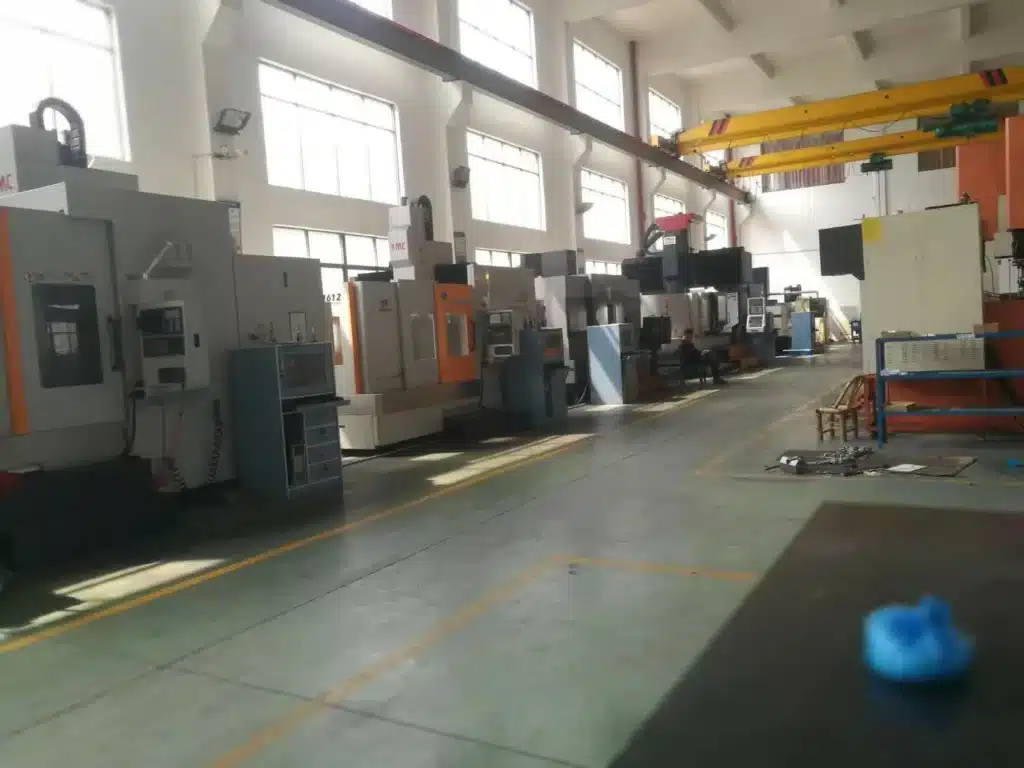
This is the point most overseas companies miss.
China’s molding factories fall into 5 distinct categories by capability and scale. Choose the wrong type and the odds of project failure run close to 80%.
These are the types you will meet most often:
| Tipo | Escala / Configuração | Capacidades e características | Prós | Contras / Riscos | Melhor para | Não se destina a |
|---|---|---|---|---|---|---|
| Pequena escala (a mais barata, a menos fiável) | 10–20 trabalhadores; 4–12 máquinas de moldagem por injeção obsoletas; sem análise de fluxo de molde; sem engenheiros | Extremely low quotes; fits toys, small housings, low-precision parts | Custo mais baixo | No quality management system; no project management; frequent delivery delays | Peças de baixo custo e produzidas em pequenas séries | Peças estruturais, peças transparentes, peças de precisão |
| Médio | 20–100 injection molding machines; full engineering team; in-house mold design | Makes most industrial parts and consumer electronics components | Amplas capacidades; geralmente estável | Capability and quality vary widely; needs careful evaluation | Cerca de 90% de compradores estrangeiros | - |
| Oficina de moldes integrada + moldagem (melhor em geral) | Strong at part design review; builds complex molds; spots risks early; stable mass production | Handles tight tolerances, undercuts, thin walls, complex structures and high cosmetic requirements | Controlo de ponta a ponta; gestão de risco rigorosa; produção em série consistente | Usually priced above standard mid-sized shops | Produtos com requisitos elevados e produção em grande escala | - |
| Fabricantes de moldes de alta precisão (automóvel/médico) | ±0,02 mm; peças transparentes; peças óticas em PC; multicavidades; canais quentes complexos | Precisão de alto nível e controlo estético | Qualidade extremamente estável | Preços mais elevados; prazos de entrega mais rigorosos e maior rigor na comunicação | Automotivo, médico, ótica, peças de alta precisão | - |
| Empresas comerciais (resultados mistos) | Excelente capacidade de comunicação em inglês; gestão de projetos; seleção de fornecedores | Bridges buyer and factory across the supply chain | Better communication; smoother project flow | Higher total cost; the wrong trader can be worse than no trader | First-time buyers; teams without engineering or local supply-chain resources | - |
For most industrial parts, a mid-sized shop or an integrated mold-and-molding plant is the right call. A trading company earns its margin only when nobody on your side can read a DFM report.
3. What Goes Wrong When You Pick the Wrong Supplier
Any one of these problems can add 3–9 months to a project or end it outright.
3.1 Erros no projeto de moldes
Design errors show up as parts that won’t release from the mold, uneven cooling, walls that are too thin, heavy ejector pin marks, and shrinkage or warpage. On T1, a part sticking in the cavity usually points to draft or polish, not to the press.

3.2 Material incorreto
Material problems come in four forms. Recycled resin, a lower grade than specified, resin with no brand at all, and unstable coloring.
The parts then crack under load, pick up fingerprint marks, discolor or age early.
❗Two failure cases
Caso 1: Substituição de material
The prototypes passed every test. At mass production, the supplier swapped PC for ABS to hold the schedule. The parts looked the same in photos, but they failed impact testing and 2,000 sets were scrapped. The COA didn’t match the batch labels. The supplier had treated the two resins as equivalent. Losses included mold rework plus the customer’s late-delivery fines.
Caso 2: Vida útil do molde sobrestimada
The quote promised 300k shots. Flash and dimensional drift started at about 80k. Maintenance records were incomplete, and the shop kept polishing gates just to keep parts coming. Lines stopped every two weeks and yield fell to 92%. Orders moved to a backup factory, which added logistics and changeover costs.
Flash that early on a tool sold for 300k shots usually means soft steel or worn shut-offs. Polishing gates fixes neither.
3.3 Redução de custos com moldes
The usual cuts are fewer cooling channels, fewer ejector pins, off-spec steel, no heat treatment and a cheap hot runner system. You pay for each one later through shorter mold life, slower cycles, higher defect rates and higher production cost.
Missing cooling lines are almost impossible to spot in photos. Ask for the cooling layout in the mold design before any steel is cut.
3.4 Qualidade instável na produção em série
Unstable output usually traces back to operator skill, old injection molding machines, process parameters nobody standardized, and loose raw material control. If the setup sheet lives in one technician’s head, your part quality walks out the door with him.
3.5 Inconsistência na qualidade entre as amostras e a produção em série
Samples often run on new machines, with premium resin, on a press the best technician has tuned. Mass production then moves to standard machines and cheaper material. The settings drift because nobody is watching that closely anymore.
3.6 Subcontratação por parte dos fornecedores
This is extremely common. A factory short on capacity, or one that can’t handle a complex structure, sends the work to a cheaper outside shop. You are rarely told.
A fábrica que se vê ≠ as instalações de produção propriamente ditas.
Ask to see your mold on a video call while it’s being machined. If they can’t show it, assume it’s somewhere else.
3.7 Questões relacionadas com as tolerâncias de montagem
You may assume the molding factory understands these:
- Tolerâncias cumulativas (acumulação)
- Folgas de montagem
- Shrinkage differences between materials
- Dimensional change after molding
Many factories don’t understand them at all.
3.8 Falta de gestão de projetos
Without a project manager, engineering drawings get missed. Tolerances, materials and structural details stay unconfirmed. Delivery dates turn into guesses.
3.9 Falta de comunicação
Even plain instructions like these get misread:
- “Acabamento da superfície: MT11010”
- “Tolerância: ±0,05 mm”
- “Requer material adequado para contacto com alimentos”
Put every one of them on the drawing and confirm each in writing. A spec that only lives in an email thread will get lost between sales and the tool room.
So judge Chinese injection molding suppliers on a system, not on price, samples and Google or Alibaba reviews. These criteria predict how a project will actually go:
- Technical competence and mold experience
- Fit with your part’s structural complexity
- Material knowledge
- Project management
- Engineering communication
- Quality control capability
- Factory transparency
- Potential for a lasting partnership
Parte 2 — Avaliar os fornecedores de moldagem por injeção da China
You need an evaluation method you can run the same way on every factory. Without one, the decision drifts back to price and gut feel, and that is how money gets lost on defects and rework.
1. Setting Up a Supplier Selection Process
A complex procurement project needs five steps.
1. Triagem inicial
Pull candidates from Alibaba, trade shows, referrals and overseas supply chain networks. Check the business license, ISO/TS certificates and major client cases. Drop anyone clearly unviable at this stage.
2. Avaliação de capacidades
- Technical capability covers DFM (Design for Manufacturing), mold flow analysis, mold design and material handling.
- Equipment means press tonnage, CNC, EDM and a CMM (Coordinate Measuring Machine).
- For the quality system, look for IQC, IPQC, FQC, OQC, FAI and CPK.
3. Avaliação de propostas
Ask for a breakdown of mold cost and of injection unit price. Then add the hidden costs, which include material markups, rework, logistics and communication delays. A quote far below the rest goes to the bottom of the pile.
4. Validação da amostra
T1 sample (initial version) → T2 sample (revised after feedback) → mass production trial (small batch run)
5. Avaliação do potencial de cooperação a longo prazo
- How fast the factory responds
- Whether its engineers can explain a problem clearly
- Delivery accuracy rate
- Project management
- Risk control
- Real willingness to work together over years, not one order
2. Initial Screening: How to Quickly Judge Factory Viability
These are the indicators to check first:
| Indicador | Método de verificação | Notas |
|---|---|---|
| Qualificação da empresa | Tianyancha / Alibaba / Materiais de exposição | Confirm injection molding and mold manufacturing are in the business scope. |
| Anos de existência | Informações oficiais sobre a inscrição | Over 5 years in business is generally preferred. |
| Número de colaboradores | Presencial/Vídeo | A plant with 50–500 employees covers most production needs. |
| Capacidade da máquina de injeção | Vídeo/Materiais de fábrica | Must match your part’s structure and size. |
| Capacidade de moldagem | Caixas de molde, aço para moldes, cavidades | Check whether they have made similar complex parts |
| Certificação ISO/TS | Verificar a autenticidade do certificado | Fake certificates exist; confirm on-site or by video |
Initial screening only has to remove obvious misfits and leave 10–15 candidates. With certificates, read the scope line, not just the logo. An ISO 9001 certificate scoped to trading says nothing about molding.
3. Avaliação da Capacidade Técnica
3.1 Capacidades de engenharia
- Do they send a Conceção para fabrico (DFM) report with the quote?
- Do they run Análise Moldflow, or only promise to?
- Can they rework wall thickness, draft angles and parting lines on your actual part?
- Have they built complex molds with hot runners and slides?
- Do they know how PP, ABS, PC, PA66 and POM behave differently in the mold?
- Will they suggest an alternative material when yours is a poor fit?
A real DFM report marks problems on your geometry with screenshots. A generic one lists design rules you could find on any website. If you want to sanity-check gate or wall questions first, our interactive injection molding tools run in the browser.
3.2 Capacidades de moldagem
- Can you verify the steel grade and where it came from?
- Does the promised mold life cover your production volume?
- What precision do their EDM and CNC machines hold?
- What does the mold warranty actually cover?
- Do the hot runner, ejector and venting layouts make sense?
- Is the mold lead time realistic, or just what you wanted to hear?
3.3 Capacidades do equipamento
- Does press tonnage fit your part size and structure?
- How do they control hot runners and multi-cavity balance?
- Can they handle polishing, spraying, silk screening and assembly in-house?
- Do they own a CMM and optical inspection equipment?
- How mature are their MES and ERP systems?
Recomendação
Ask for a live video walk-through and watch a press running your type of part. Pictures and brochures prove nothing.
4. Quotation Evaluation: Breaking Down the Price and Avoiding Low-Price Traps
Split every quote into its parts:
Mold cost = steel + mold base + CNC/EDM + design + assembly + profit
Unit price = material + molding cycle + labor + post-processing + packaging + defect loss
4.1 Custos ocultos
- Material markup, which is common on transparent parts and engineering plastics
- Mold modification fees
- Rework to fix mistakes
- Logistics and tariffs
- Delays caused by misunderstandings or translation problems
4.2 Como evitar as armadilhas dos preços baixos
A quote well below market, around 30% lower for example, is a red flag. Something in the mold steel or hot runner has probably been downgraded. An undersized press stretches cycle time and widens part variation. And a shop with no quality process makes up the difference in rework.
When you request quotes, ask for steel grades, labor hours and expected mold life in writing. A supplier who won’t itemize these is hiding something.
5. Verificação de amostras (T1 → T2 → Lote pequeno)
5.1 Amostra T1
On T1, check dimensions against the drawing and look closely at appearance and finish. Measure shrinkage and warpage after the parts have stabilized, not straight off the press.
5.2 Amostra T2
The mold gets modified based on T1 results. Then dimensions and function are checked again.
5.3 Lote pequeno
- Confirms mass production is stable
- Shows the real defect rate
- Precisão das cores
- Gloss level across the run
Always run a small batch of at least 50–200 pieces before mass production. It is the only real test of whether the factory can repeat itself.
6. Potencial para uma colaboração a longo prazo
Technical skill is half of it. Watch how the factory behaves on these points:
| Avaliação | Observação |
|---|---|
| Velocidade de resposta | Response time on Email, WeChat, Skype, WhatsApp. |
| Competências de Engenharia | Capacidade de compreender projetos complexos e requisitos de tolerância |
| Precisão na entrega | Consultar encomendas anteriores e pequenas produções de teste |
| Gestão de Projetos | Dedicated people tracking each production stage |
| Controlo de riscos | How they handle mold changes, material replenishment and rework |
| Disponibilidade para uma cooperação a longo prazo | Aceitação do Acordo de Confidencialidade (NDA) e dos contratos relativos à propriedade dos moldes |
A long-term partner beats a short-term low price almost every time.
7. Compreensão de documentos técnicos
Four documents tell you more about a factory than any sales call. If one of them is new to you, our Centro de Formação em Moldagem por Injeção explains each.
1. Relatório de análise do Moldflow
Look at weld lines, shrink marks, bubble locations and cooling uniformity. This report tells you whether the mold design is reasonable. A weld line on a cosmetic face is far cheaper to move now than after T1.
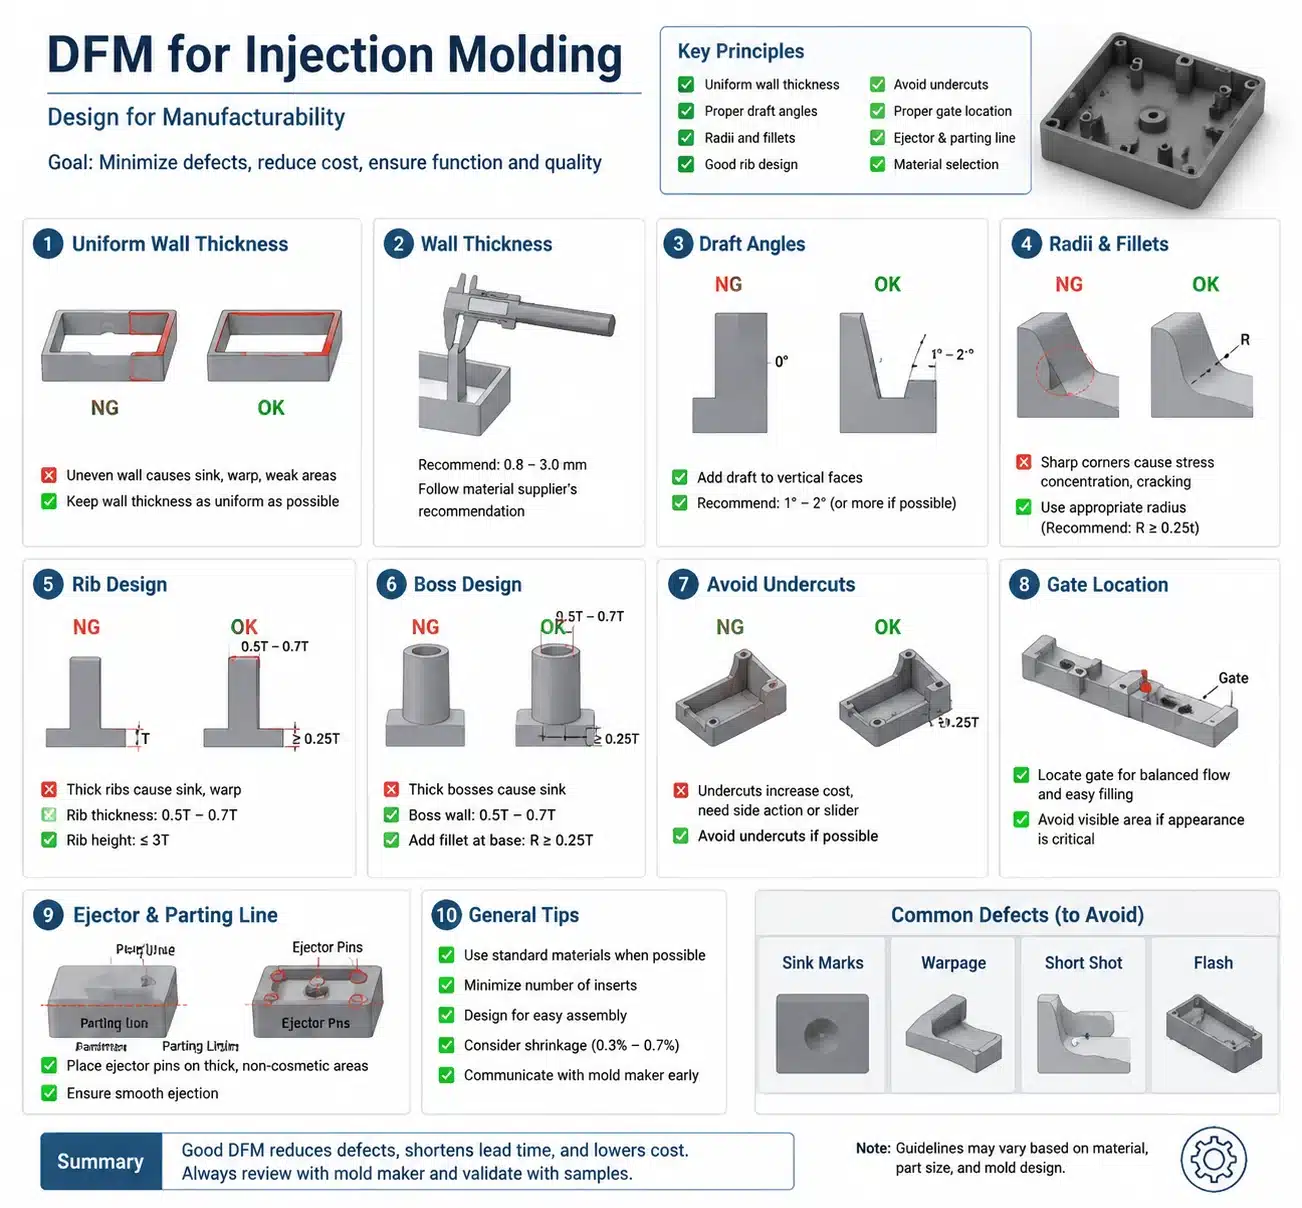
2. Relatório DFM (Conceção para Fabrico)
- Espessura da parede
- Ângulos de inclinação
- Raios
- Tolerância
Use it to judge whether the part can actually be produced as drawn.
3. Exemplo de relatório de ensaio
This one covers dimensional deviation, tolerances, material properties, surface finish and color. It validates what the factory can really do, so read the out-of-tolerance rows first.
4. Relatório de inspeção da CMM (Máquina de Medição por Coordenadas)
Check critical dimensions and the tolerance on mating holes. If those numbers move between samples, mass production won’t be controllable.
8. Avaliação sistemática
Exemplo de questionário para fábricas (pronto a utilizar)
- How many injection molding machines do you run, and what is each one’s clamping tonnage?
- What is your mold manufacturing capability? Which steels do you use, and what life do you expect?
- Realizam análises de DFM ou Moldflow?
- Do you have IQC, IPQC, FQC, OQC, FAI or CPK processes?
- What is your typical mold lead time? How do you handle delays?
- Is there a limit on sample modifications?
- Can you run a small batch trial?
- Will you sign an NDA?
- What are your mold ownership terms?
- Can you share references or case studies from previous clients?
Exemplo de lista de verificação de controlo de qualidade
- Appearance: warping, bubbles, scratches
- Dimensions: critical dimensions against tolerance
- Materials: color, gloss, certifications
- Molds: ejector marks, shrink marks, parting lines
- Batch stability: dimensions, weight, defect rates
Send the questionnaire to every shortlisted factory and score the answers against the checklist. Comparing five suppliers then takes an afternoon.
9. Processo de avaliação de fornecedores científicos
Run this process and most bad suppliers drop out before you pay a deposit. Low-price and mold traps surface in the quote breakdown. Weak technical skill and thin quality systems show up in the DFM report and the small batch. Mass production feasibility gets proven on real parts, not promises.
An NDA or mold ownership clause is a quiet test of long-term intent. A factory that resists either one is telling you how the partnership would go. What remains is a short list you can choose from on fit, with price as one factor among several.
Parte 4 — Controlo de Qualidade e Estabilidade da Produção
A capable supplier without a working Quality Control (QC) system will still ship bad parts. This part covers IQC, IPQC, FQC, OQC, FAI and CPK, and what to check at each stage.
1. Why Quality Control Matters More Than Supplier Selection
Picking a good factory is step one. Mass production still carries real risk:
- Samples look fine, then production batches vary.
- Raw material batches differ in ways that shift dimensions, color or strength.
- Process parameters that were never standardized cause shrinkage or warpage.
- Undertrained operators create cosmetic defects.
- Mold wear slowly pushes critical dimensions out of tolerance.
Production stability depends on technical capability, QC process, standard work, material control and mold maintenance together. On a long run, the first sign of wear is usually flash at the shut-offs, well before any dimension drifts out.
2. Processos comuns de controlo de qualidade nas fábricas chinesas de moldagem por injeção
Most Chinese molding factories use these stages, under the English abbreviations used in international procurement:
| Fase de Controlo de Qualidade | Nome completo | Objetivo principal |
|---|---|---|
| IQC | Controlo de Qualidade na Entrada | Inspection of raw materials, auxiliary materials and purchased components |
| IPQC | Controlo de qualidade durante o processo | Monitoring critical dimensions and process parameters during production |
| FQC | Controlo de Qualidade Final | Inspeção final dos produtos acabados antes do envio |
| OQC | Controlo de Qualidade na Saída | Pre-shipping check of packaging, quantity, function and appearance |
| FAI | Inspeção do primeiro artigo | Checks the first article against design requirements for mold and process |
| CPK | Índice de Capacidade do Processo | Measures process capability and batch stability |
Done properly, structured O controlo de qualidade garante que cada fase of production has its own checkpoint. Problems then get caught where they start.
2.1 IQC — Controlo de Qualidade na Entrada
IQC confirms raw materials and purchased components meet spec before they reach a press. Inspectors check:
- Material grade, supplier and batch number
- Color, gloss and physical performance
- Ratios of reinforcement and additives
- Pellet integrity and size
- Chemical or physical tests when needed
Bad resin destabilizes everything downstream. IQC is the first line of defense, and it is cheap compared with scrapping a batch.
2.2 IPQC — Controlo de Qualidade durante o Processo
IPQC catches problems mid-run, before a whole batch is rejected. Inspectors pull 1–5 pieces per batch for critical dimensions. They track temperature, pressure, holding time and cooling time on the press, plus mold temperature and cycle. They also confirm operators follow the SOP on critical steps and watch for warpage, shrink marks and bubbles.
2.3 FQC — Controlo de Qualidade Final
FQC confirms every product meets spec before shipment.
- Appearance, checked for scratches, bubbles and warpage
- Critical dimensions measured by CMM or calipers
- Function tests such as assembly, durability and torque
- Packaging, covering quantity, labels and electrostatic protection
Sampling alone isn’t enough here. FQC should cover 100% of critical dimensions if you want consistency your customers can rely on.
2.4 OQC — Controlo de Qualidade na Saída
OQC is the last look before parts leave. It reconfirms packing quantity, appearance, function and packaging integrity. It also checks the shipping documents, which usually means the COC, MSDS, Packing List and Test Report. Many customer complaints trace back to paperwork or packaging, not the parts themselves.
2.5 FAI — Inspeção do Primeiro Artigo
FAI proves the mold, process and parameters are right before volume starts. The first article gets compared with the drawing or 3D file, and every critical dimension is measured. Mold life and tolerances are reviewed. Then the customer signs off on the samples.
Many low-cost factories skip FAI. That single shortcut causes a large share of the production disasters I get called in to fix.
2.6 CPK — Índice de Capacidade do Processo
CPK shows whether the process can hold critical tolerances over time. Factories report Cp and Cpk, usually on hole positions, thickness and assembly dimensions. The statistics tell you whether the process needs work. Automotive, medical and optical customers treat CPK as mandatory.
A factory without CPK data has no way to control dimensional variation in mass production.
3. Verificação das capacidades de controlo de qualidade da fábrica
Start with paper. Ask for the QC process documents, check that each step has an SOP, and confirm a named person owns each stage.
Then audit on-site or by video:
- Watch IQC sample testing on incoming material
- Review how IPQC samples during a live run
- Read the FQC records, not just the blank forms
- Observe OQC packing
- Request FAI reports and small batch data, and check they are complete and authentic
- Compare batch data against statistical records
Finally, run a trial. A small batch of 50–200 pcs with 5–10% sampling, or 100% checks on critical dimensions, tells you more than any audit. Look at rework rates and standard deviations in the results. On-site audits plus real data are the combination that predicts stable mass production.
4. Processo de execução completo, desde a amostra até à produção em série
4.1 Fase de amostragem
- T1 verifies the factory can mold the part at all.
- T2 validates the modified samples.
- Stakeholders sign the sample confirmation.
- A small batch trial of 50–200 pieces tests production capability.
- Full IQC, IPQC and FQC inspections run on that batch.
- CPK and yield rates are confirmed against the standard.
O nosso 20L paint bucket mold case study follows a real tool through this path, from T1 to mass production.
4.2 Preparação para a produção em série
- Confirm the mold has been maintained and is ready.
- Train operators on the critical processes.
- Lock standard settings for temperature, pressure, cooling time and ejection speed.
- Confirm the material batch meets spec.
4.3 Fase de produção em massa
- Sample critical dimensions from every batch.
- Run full FQC inspection.
- OQC does a final review before shipment.
- Record and archive all QC data.
4.4 Monitorização da qualidade a longo prazo
- Plan mold life and schedule maintenance against it.
- Update process parameters as production data comes in.
- Keep verifying material suppliers.
- Collect customer feedback and feed it back into the process.
5. Ferramentas práticas e modelos
These templates make quality control measurable and auditable:
- Lista de verificação de controlo de qualidade (dimensões, aspeto, funcionamento)
- Modelo de Inspeção do Primeiro Artigo (FAI)
- Registo de Estabilidade do Lote (Cálculo do Cpk)
- Ficha de análise da taxa de retrabalho e de defeitos
What to Insist On Before Approving Mass Production
If a supplier pushes back on any of these, treat it as a capability gap, not a negotiating position.
- The full QC chain of IQC, IPQC, FQC, OQC, FAI and CPK, with records you can see.
- A small batch trial before volume. It finds problems while they are still cheap.
- Recorded process data, so drift shows up in numbers before it shows up in complaints.
- A mold maintenance schedule and documented material control.
- A price that reflects all of the above. Real QC capability is worth more than a low quote.
Part 5 — Long-Term Collaboration
Once a supplier passes sampling, the job shifts to keeping them good. A factory that already knows your parts, your tolerances and your quirks becomes more valuable every year. Switching resets all of that.
1. O valor da colaboração a longo prazo
Choosing a supplier is a strategic commitment, not a single transaction.
- Long relationships open room to negotiate better pricing and payment terms.
- Rework drops as the factory learns your products and processes.
- Urgent orders, mold changes and special material requests move faster.
- Trust lowers the risk of shortages on critical components.
- A committed supplier will join in on design changes, material selection and process improvements.
The lowest first price is rarely the lowest total cost.
2. Elementos-chave da gestão de fornecedores
2.1 Gestão de contratos e acordos
- An NDA covering mold designs, formulations and process documents, so your IP stays protected.
- Mold ownership clauses that also settle maintenance, depreciation and what happens at end of life.
- Delivery terms (FOB / CIF / DDP) that leave no room to argue over shipping costs.
- Quality terms naming QC standards and first article requirements, plus defect rates, rework costs and compensation.
- Phased payments at T0 (contract signing), T1 (mold completion) and pre-mass production. Never pay it all upfront.
Mold ownership is the clause buyers regret skipping most. Without it, moving your tool to another factory later becomes a negotiation you will lose.
2.2 Indicadores-chave de desempenho (KPI) e gestão do desempenho
Track supplier performance with numbers, not impressions:
| Indicador KPI | Descrição | Método de medição |
|---|---|---|
| Taxa de entrega pontual | Pontualidade nas entregas | Data de entrega efetiva vs. data de entrega prevista |
| Taxa de rendimento | Qualidade do produto na primeira produção | Taxa de retrabalho e resultados das inspeções |
| Resposta técnica | Rapidez na resolução de problemas de engenharia | Tempo médio de resposta |
| Eficiência na comunicação | Rapidez nas respostas por e-mail/WeChat/Skype | Tempo médio de resposta |
| Reclamações relativas à qualidade | Problemas identificados pelos clientes ou a nível interno | Número de reclamações por cada 1 000 unidades |
Review KPIs quarterly or twice a year. Tie the results to pricing and contract terms, or the review becomes a formality.
2.3 Mecanismo de partilha de riscos
Mold damage is the first thing to settle. The factory should cover significant damage beyond normal wear. Your side supplies the materials or process guidance the factory needs.
Material prices move. The contract should spell out approved upgrades and alternatives, and how price swings get shared in a reasonable split.
Urgent orders need their own terms. Agree expedite fees or priority production slots in advance, and write down who is responsible for what.
When both sides carry part of the risk, both sides want the project to work. That alignment is what keeps a partnership stable.
3. Melhores práticas para aquisições no estrangeiro e comunicação com fornecedores
3.1 Gestão de Projetos
Name one project manager on your side to own the whole process. That person handles communication, progress tracking and document archiving. Set milestones for each phase of design, mold, samples and mass production.
3.2 Manutenção das relações com os fabricantes
- Hold regular video or on-site meetings
- Bring the supplier into mold and sample reviews
- Give feedback fast, including when something went well
- Reward good performance with priority orders or volume discounts
3.3 Colaboração em processos e conceção
- Share DFMEA (Design Failure Mode and Effects Analysis) and DFM reports both ways.
- Ask the factory to propose improvements it can actually deliver.
- Prove each improvement on samples or a small batch before rolling it out.
Two-way communication prevents most of the silos and misunderstandings that derail projects. I would rather get an awkward question from a supplier on day one than a surprise on T1.
4. Otimização contínua da cadeia de abastecimento
A long relationship should improve the supply chain itself, not just renew the contract:
- Work with the factory and its resin suppliers to secure stable material sources, with unified batch management to cut variation.
- Schedule mold maintenance, lubrication and cleaning, and track mold life to predict replacement. Tecnologia de Fabrico de Moldes publishes practical guidance on maintenance routines.
- Agree production schedules for peak periods, and discuss equipment upgrades or expansion.
- Build a QC database and review tolerances, rework rates and complaints on a fixed cycle.
5. Where to Start if You Only Fix Three Things
Get the contract right first. That means an NDA, mold ownership and quality terms.
Next, measure the supplier with KPIs and connect the results to rewards and penalties. Then make sure a named project manager runs regular reviews with transparent feedback on both sides.
Risk sharing on molds, materials and urgent orders comes after that. So does ongoing work on material control, mold maintenance, capacity and quality data. Short-term low prices can’t buy any of this. A stable supply chain is built on price, quality, speed and trust together.
Before You Send Your First RFQ
Send the same 3D file to your two strongest candidates and ask for a DFM report before any price. The supplier who comes back with questions about your draft angles and tolerances is usually the one worth paying more for.
Want an engineer’s second opinion on a China injection molding supplier’s quote or DFM report before you commit?
Entre em contacto connoscoTo turn this checklist into a quote, start with our moldagem por injeção na China service.

